Maintenance planning · risk based · record ready
Build the maintenance program from the installed blister machine, approved procedures, operating history and product risk—not from a universal daily, weekly or annual calendar.
This guide separates operator checks, cleaning, planned technical work, changeover verification, escalation and return-to-service evidence for thermoform and cold-form blister equipment.
What should a blister machine maintenance checklist include?
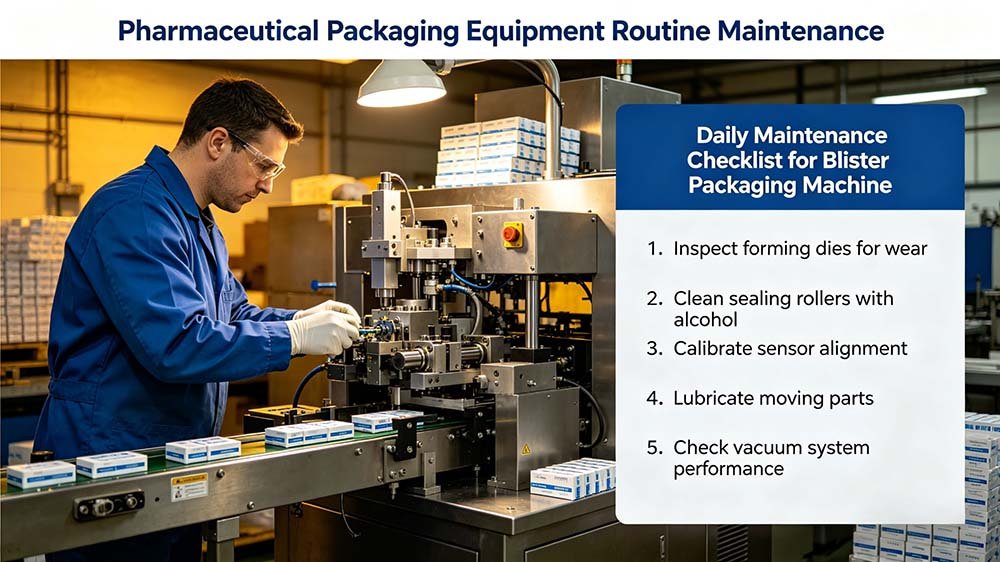
The checklist should follow the actual machine path: material unwind, forming, product feeding, inspection, lidding, sealing, registration, perforation and cutting, reject handling and discharge. Add the utilities, guarding, extraction, coding, data, vision and downstream interfaces installed on the specific line. A generic checklist that omits a supplied module can leave a real failure mode outside the maintenance program.
Each task needs more than a tick box. State the safe machine condition, approved method, responsible role, tools or materials, expected result, action when the result is unacceptable and the record to retain. Separate observation from intervention: an operator may identify a leak or abnormal sound, while isolation, diagnosis, repair and release may require maintenance, engineering or quality roles.
Confirm configuration, utilities, guarding, cleanliness, tooling, recipe, inspection and reject readiness.
Reconcile materials, clean safely, inspect as-found condition and record alarms, damage or residue.
Inspect, lubricate, adjust, calibrate or replace only against approved instructions and limits.
Verify assembly, settings, functions, inspection, accepted packs and any qualification impact.
Safety boundary: only trained and authorized personnel should service the machine. Apply the site’s approved energy-isolation procedure before entering guarded areas or working on electrical, pneumatic, thermal or moving components. The checklist must not invite cleaning, lubrication or adjustment of moving equipment.
How should maintenance frequency be set?
Start with mandatory instructions in the current machine and component manuals. Translate those instructions into operating hours, cycles, calendar intervals or event-based tasks as appropriate. Then use site experience—breakdowns, alarms, reject trends, wear measurements, environmental exposure, cleaning history and product residue—to decide whether a task needs closer observation or a justified interval change.
Daily, weekly, monthly and annual headings can organize work, but they are not universal technical limits. Two blister lines can require different intervals because they run different materials, batch patterns, products, shifts, tooling and environments. A line with abrasive dust or frequent format changes may need different inspection points from a line running one clean, stable format.
| Frequency input | Question to answer | Evidence to retain |
|---|---|---|
| Manual requirement | What does the current machine or component instruction require? | Manual revision, task reference and prescribed interval or condition. |
| Use profile | How many hours, cycles, batches, starts, stops and format changes occur? | Meter readings, batch history and changeover log. |
| Condition trend | Are wear, temperature, vibration, leakage, alignment or alarms changing? | Inspection results, measurements, photographs and alarm history. |
| Product and environment | Do dust, residue, cleaning agents, humidity or temperature add risk? | Risk assessment, cleaning observations and environmental records. |
| Quality impact | Could deterioration affect forming, feeding, sealing, inspection, coding or rejection? | Defect/reject trends, deviations and accepted-pack results. |
Swipe horizontally to view the full table.
Pre-shift inspection before production release
A pre-shift check asks whether the line is in the approved condition to start—not whether it merely powers on. Confirm the correct format parts, product path, materials, recipe and inspection setup before the first accepted pack is released.
| Area | Check | Record or response |
|---|---|---|
| General condition | Look for loose parts, damaged cables, residue, foreign material, leakage or guards out of position. | Do not start when a safety, contamination or damage risk is unresolved. |
| Utilities | Confirm electrical supply, compressed air, cooling water, extraction and other project utilities. | Record abnormal indications and assess them against approved limits. |
| Tooling and web path | Confirm forming, sealing, cutting and guide parts match the released setup and are correctly identified. | Record tooling or format revision where required. |
| Materials | Verify forming web, lidding material, print/code data and batch identification. | Resolve wrong, damaged or unidentified material before loading. |
| Guards and safety | Complete the approved accessible check of guards, interlocks and emergency functions. | Stop and escalate any failed safety function. |
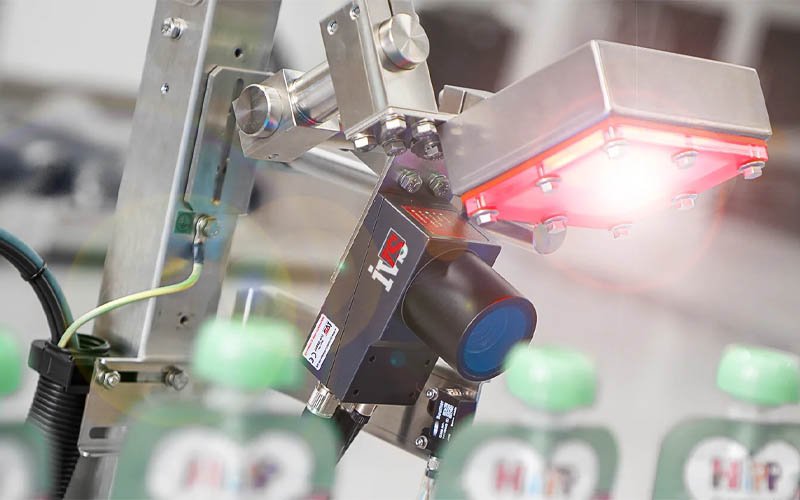
| Inspection and reject | Confirm sensors, cameras, reject bins, reject confirmation and challenge items are ready. | Document the challenge result required by the approved setup. |
| HMI and recipe | Verify the approved recipe, authorized access and required prior-batch clearance. | Record the selected recipe or configuration identifier. |
Swipe horizontally to view the full table.
Post-shift cleaning and as-found condition
The post-shift check preserves evidence before adjustment or cleaning removes it. Record unusual noise, vibration, heat, odor, alarms, repeated stops, web tracking, reject behavior and visible wear. Account for remaining product, printed materials and rejects under the approved reconciliation and line-clearance procedure.
- Remove product and packaging-material residue from accessible feeding, forming, sealing, cutting and discharge areas using the approved method.
- Inspect product-contact parts and collection areas for trapped material, damage or wear.
- After safe cooling and isolation, inspect forming and sealing surfaces for buildup, scoring, contamination or foreign material.
- Inspect cutters and perforation tooling without touching exposed edges; refer defects to qualified personnel.
- Check rollers, guides and web-contact surfaces for adhesive, foil fragments, dust or edge damage.
- Return removed parts, guards, tools and cleaning materials to controlled locations and document line status.
Planned mechanical maintenance by machine system
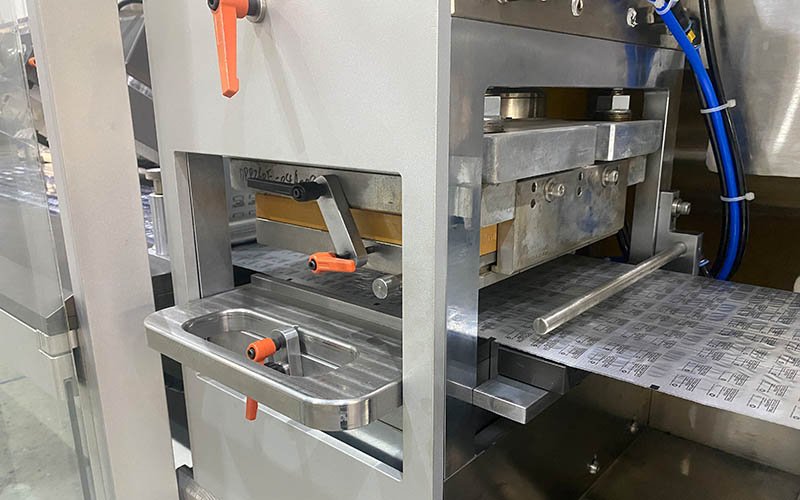
Planned work should connect the task to a failure mode and a defined response. “Inspect bearing” is incomplete unless the method, access, expected condition and escalation criteria are understood. Lubricants, cleaning agents, replacement parts and fasteners should match controlled instructions and material requirements.
| System | Planned check | Escalation trigger |
|---|---|---|
| Web transport | Rollers, guides, tension components, chains, belts and alignment. | Tracking drift, edge damage, slip, dust or recurring web alarms. |
| Forming station | Heating surfaces, forming tooling, cooling connections, seals and fasteners. | Uneven cavities, leakage, temperature instability or visible damage. |
| Feeding | Brushes, tracks, chutes, vibratory parts, sensors and retainers. | Empty cavities, chipped product, jams or unstable feed behavior. |
| Sealing station | Platen or roller condition, bearings, pressure system and temperature sensing. | Seal variation, foil marking, noise, heat drift or reject trend. |
| Indexing and drive | Motors, couplings, gears, cams, bearings and approved lubrication points. | Position error, backlash, vibration, heat rise or abnormal sound. |
| Cutting and discharge | Cutters, perforation, registration, guides, conveyors and transfer points. | Burrs, incomplete cuts, registration drift or transfer jams. |
Swipe horizontally to view the full table.
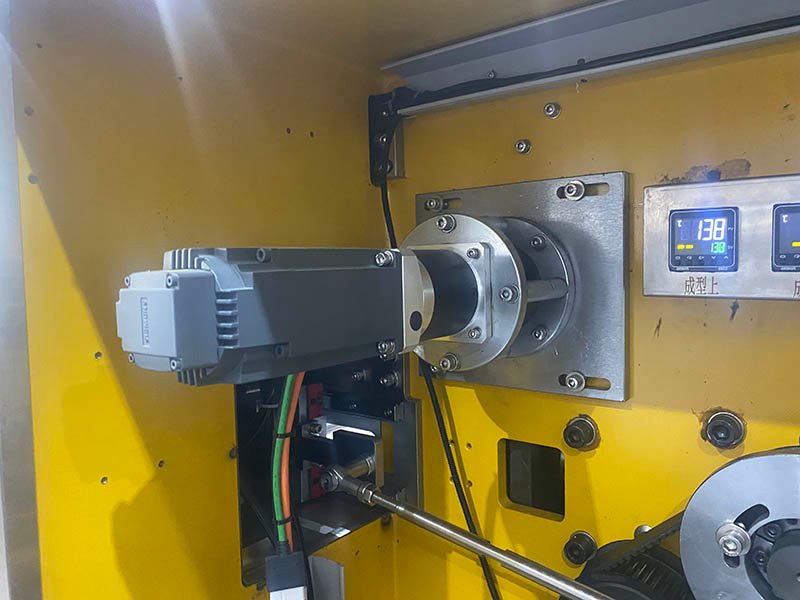
Control spare parts, lubricants and maintenance materials
A replacement part is not equivalent merely because it fits. Identify the approved part number, revision, material or rating, function and any parameter that affects safety, product contact, motion, temperature, measurement, inspection or control. When an alternative is proposed, assess it through the site’s technical and change-control process before installation rather than treating it as routine stock substitution.
Store tooling, sensors, belts, seals, bearings, cutters and electronic parts in conditions that protect their usable state. Preserve identity and traceability where required, separate serviceable from rejected items and define how repaired or sharpened components return to approved inventory. For long-lead or obsolescence-sensitive components, the project team should agree which strategic spares, drawings, settings or supplier notices are included.
Lubricants, cleaning agents, wipes and other maintenance materials also need control. Use only materials permitted by the applicable machine and site procedures, apply them at the approved point and quantity, and prevent unintended product or packaging contact. Record introduced material when the approved maintenance procedure or quality system requires traceability.
At procurement, request a component-level recommended-spares list that distinguishes commissioning items, routine wear parts, critical downtime spares and optional stock. Confirm part identification, supplied quantity, storage needs, replacement method and what acceptance check follows installation. A generic “spares included” statement is not a maintainability plan.
Electrical, pneumatic, control-system and backup checks
Control-system maintenance must preserve the approved configuration and data boundary. Inspect cabinet filters, fans, cooling paths, cables, connectors, sensor mounts and pneumatic tubing under authorized procedures. Review recurring alarms instead of clearing them without assessing the cause.
- Confirm critical instruments remain in their calibration program and identify items approaching their due date.
- Inspect pneumatic tubing, fittings and pressure indications for damage, looseness or leakage.
- Check cabinet cooling and signs of overheating without bypassing electrical-safety controls.
- Back up approved recipes and configuration only through the site’s controlled access, version and storage procedure.
- Test safety, alarm, inspection and reject functions using the method and frequency defined in the approved program.
- Document unauthorized, unexplained or failed configuration changes as deviations rather than normal adjustments.
Checks after maintenance, repair or format change
Maintenance can alter alignment, tooling position, guides, feeder settings, recipes, coding and inspection. Before routine production resumes, confirm the machine is correctly reassembled, guards and services are restored, tools and parts are accounted for, and the intended configuration is selected.
Use representative product and materials where the intervention can affect finished-pack quality. Verify the affected function and its downstream consequence: a forming adjustment may require cavity checks; a sealing intervention may require the approved seal or integrity method; a sensor or reject repair should include a defined challenge; a control change may require configuration and data checks.
Stop conditions that should not become routine adjustments
Repeated adjustment can hide a deteriorating condition and erase evidence needed for root-cause work. Stop and escalate when there is a failed guard or interlock, exposed electrical hazard, uncontrolled leak, damaged tooling, unexplained contamination, repeated reject-system failure, loss of required calibration status, abnormal heat or vibration, or a change that may affect the qualified state.
For recurring forming, feeding, sealing, registration or control symptoms, use the blister packaging machine troubleshooting guide to organize containment, evidence and fault isolation before changing multiple settings.
Minimum maintenance record and return-to-service evidence
The useful record shows what condition existed before intervention and why the machine was acceptable afterward. A work order marked “completed” does not by itself show the configuration, test or release decision.
| Record field | Why it matters | Typical evidence |
|---|---|---|
| Asset and module ID | Links the work to the installed machine and affected station. | Machine ID, serial/model, module and location. |
| Date and use status | Supports interval control and event reconstruction. | Date, time, hours/cycles, batch or downtime reference. |
| Approved task | Shows which instruction governed the work. | SOP, manual, work instruction and revision. |
| As-found condition | Preserves the symptom before adjustment or replacement. | Observation, measurement, alarm, sample or photograph. |
| Intervention | Provides traceability for work and introduced materials. | Repair, setting, part ID, lubricant or cleaning agent. |
| Post-work test | Shows whether the affected function met its approved criterion. | Test method, result, samples, reject challenge or measurement. |
| Exception reference | Connects unresolved findings to formal control. | Deviation, CAPA, change control or open work order. |
| Release decision | Identifies who authorized return to the next state. | Performer, reviewer, quality involvement and status. |
Swipe horizontally to view the full table.
When does maintenance affect calibration, change control or qualification?
Preventive maintenance does not replace calibration, and a successful repair does not automatically prove the full process remains qualified. Assess impact when work changes a critical component, software or recipe configuration, calibrated instrument, tooling geometry, operating range, inspection logic, data path or an approved design feature.
The depth of post-maintenance testing should follow documented risk and the affected function. Some tasks may need only an inspection or functional check; others may require calibration, change control, additional challenge testing or partial requalification. Use the DQ, IQ, OQ and PQ blister packaging guide to define the evidence boundary rather than labeling every intervention the same way.
Who should own each maintenance decision?
Operators
Perform trained inspections, cleaning and setup checks; record observations; stop and report conditions outside the approved procedure.
Maintenance and engineering
Diagnose, isolate, repair, measure and test within authorized technical procedures; identify configuration or qualification impact.
Quality and system owners
Define review and release responsibilities for deviations, calibration, change control, records and qualified-state decisions.
Convert this guide into a site-specific SOP
- Map the installed scope. List the exact machine, modules, utilities, tooling, inspection, coding, reject and downstream systems.
- Import controlled requirements. Use current manuals, approved drawings, component instructions and site procedures.
- Rank failure modes. Consider personnel safety, product quality, contamination, data and production consequences.
- Define every task. Name the safe state, method, tools, competence, expected result, response and record.
- Define release authority. State who can return the machine to setup, testing or routine production and when quality review is needed.
- Trend and improve. Review breakdowns, repeat adjustments, parts use, overdue work, defects and downtime; revise intervals only with documented justification.
When buying equipment, include access, cleaning, format-part handling, diagnostics, spare-parts information and maintenance documentation in the URS. Review the available blister packing machine configurations and the blister tooling and mold design guide before freezing the project boundary.
Primary regulatory and technical references
These sources define important equipment and documentation expectations but do not prescribe one universal blister-machine maintenance interval.
- 21 CFR 211.67: Equipment cleaning and maintenance
- 21 CFR 211.68: Automatic, mechanical and electronic equipment
- European Commission: EudraLex Volume 4 GMP guidelines
This article is an engineering planning guide. It does not replace the current machine manual, equipment-specific safety assessment, approved site SOP, regulatory interpretation or quality-unit decision.
Continue the maintenance decision
Frequently asked questions
How often should a blister packaging machine be maintained?
Use the current machine manual, approved site SOP, operating hours or cycles, risk assessment, environment and observed condition. Daily inspection and cleaning may be appropriate, but mechanical, electrical, calibration and replacement intervals are machine and site specific.
What belongs on a daily blister machine maintenance checklist?
A daily or per-shift list can cover visible condition, cleanliness, leaks, utilities, guards, tooling and web path, approved recipe, inspection and reject readiness, plus alarms or abnormal noise, heat and vibration. It should state the response when a check fails.
Can operators perform all maintenance tasks?
No. Operators should perform only tasks covered by their training and approved procedures. Work involving energy isolation, electrical systems, guarded mechanisms, tooling alignment, software configuration or calibrated instruments may require qualified maintenance or engineering personnel.
What should be checked after replacing a critical component?
Document the as-found condition, component identity and work performed. Verify assembly and the affected function, then assess calibration, configuration, change control, challenge testing and requalification according to the component’s impact.
Does preventive maintenance replace calibration?
No. Maintenance and calibration have different purposes. Instruments that affect an approved result should remain in the applicable calibration program even when the surrounding machine receives preventive maintenance.
Should PLC recipes and backups be part of maintenance?
Controlled backup can be appropriate when recipes or configuration support regulated operations. Define authorized access, version identity, secure storage, restore capability and change control in the applicable site procedure.
When can maintenance require requalification?
Assess requalification when work may affect an approved design, critical component, calibrated instrument, software or recipe configuration, tooling geometry, operating range, inspection or reject logic, data path or finished-pack quality. The response should be risk based and documented.
What maintenance records should be retained?
Retain the asset and module identity, date and use status, approved task reference, as-found condition, intervention and introduced parts or materials, post-work test and acceptance result, exception reference, performer, reviewer and release status required by the quality system.
Define the maintenance boundary before machine selection
Share the product and material route, machine modules, operating pattern, cleaning boundary, changeover profile, inspection scope and required maintenance documents. HIJ can review which access, diagnostics, spare-parts and acceptance questions belong in the project specification.
Discuss My Maintenance Scope The final maintenance program and release decision remain within the buyer’s approved procedures and quality system.