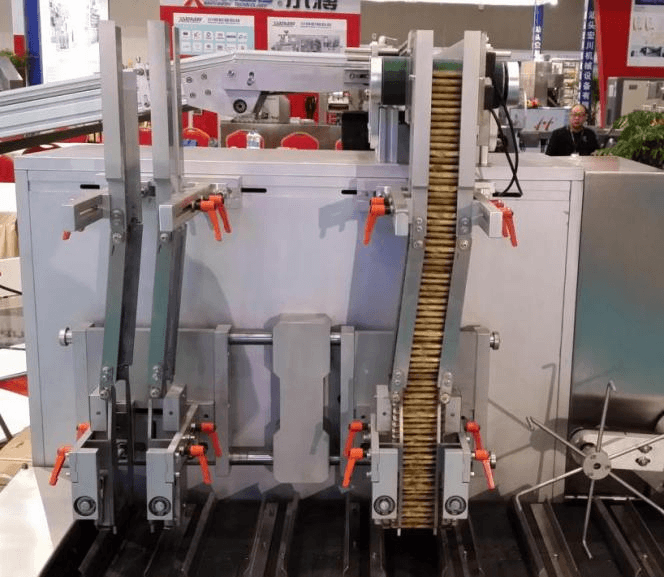
Equipment selection · Retail carton or shipping case
A cartoner packs a product or product group into a folding carton, usually the retail pack. A case packer groups and loads packs into a shipping case. Choose by the package you need to make: retail carton, transport case, or both in sequence—not by which machine has the larger speed number.
This comparison helps factory managers, engineers and purchasing teams define the right equipment category before requesting a quotation. It covers already packed products such as bottles, blisters and pouches, not filling their contents or manufacturing cardboard.
Cartoner vs case packer: start with the finished package
The useful distinction is the job the package performs. A folding carton may present one bottle, a blister with a leaflet, or a counted group of sachets as a saleable unit. A shipping case groups packs for handling and distribution. In a common two-stage arrangement, the cartoner makes the retail cartons and the case packer loads several of those cartons into an outer case.
| Selection question | Cartoner | Case packer |
|---|---|---|
| What leaves the process? | A loaded folding carton, with its specified closure. | A loaded shipping case; closure is included only when specified. |
| What is loaded? | A product, a counted group, and any specified insert. | A group of retail cartons or suitable primary packs. |
| What defines the format? | Product presentation, carton drawing, count and closure. | Pack pattern, case drawing, orientation, layers and closure. |
| How is output stated? | Usually cartons/minute, with the product count identified. | Usually cases/minute, with the contents per case identified. |
| Which details need confirmation? | Feeding, insertion, leaflet handling, checks and rejection. | Grouping, case supply, loading, dividers, closing and checks. |
Names alone are unreliable. “Carton packer” or “box packing machine” may describe either task in a supplier catalogue. Send a photograph of the open and closed pack and a drawing showing its contents. Ask the supplier to describe the incoming material and delivered package in plain terms.
Material is a clue, not the sole rule. Folding cartons commonly use paperboard and shipping cases commonly use corrugated board, but display-ready cases, trays and wraparound formats complicate that shortcut. The approved pack drawing and required function are more precise than a label such as “secondary packaging.”
Do you need a cartoner, a case packer, or both?
Work backwards from the package your customer or distribution operation requires. The three routes below are planning options, not claims that every product or machine can run all three.
Route A: product → retail carton
Investigate a cartoner when the missing operation is placing the product into its individual saleable carton. Examples include a bottle with an insert or a defined blister count in a printed box. If the outer shipping cases are packed elsewhere or remain manual, case-packing automation is outside this initial purchase.
For the available equipment categories, start with the HIJ cartoning machine range. A retail carton does not automatically imply automatic product feeding: describe which tasks operators will still perform.
Route B: primary packs → shipping case
A retail carton is not mandatory in every packaging route. Suitable sealed pouches, bottles or other primary packs may be grouped directly into an outer case when the approved product and distribution specification allows it. The case-packing equipment then needs to handle those packs, not an assumed intermediate carton.
As an industry example, Syntegon's case-packing overview describes handling both primary pack formats and folding cartons. This demonstrates the distinction between packing routes; it does not establish that a particular HIJ configuration handles every listed format.
Route C: product → retail carton → shipping case
Both machines are relevant when the required finished presentation has these two packaging levels and both loading operations are to be automated. The cartoner and case packer are complementary stages, not competing alternatives. Confirm that the case packer receives cartons in the orientation and condition it needs.
A shelf-ready outer pack can also serve a display function. Specify how it must be opened and presented, rather than assuming that “retail” always means the inner carton. Packaging design comes first; the machine category follows that design.
The loading task matters more than a similar-looking conveyor
A cartoner may need to open a folding carton, support it, present the product correctly and insert the product without damaging either. A case packer must establish the specified group and load it into the outer case. Those tasks involve different tooling and product handling even when both machines use a side-loading motion.

For a cartoner, provide the product dimensions and presentation, carton opening, insertion direction, number of items and any leaflet or internal support. Ask how a fragile edge, projecting seal or loose group will be controlled. The cartoner infeed guide covers that machine-level selection in more detail.
For a case packer, provide a drawing of one complete layer and the full case. Identify which face of each pack points up, how many layers are required, and whether dividers, pads or separators are present. A picture of an empty case is not enough to define a loading pattern.
Ask the supplier to explain the proposed movement with your samples. Side loading, top loading and other arrangements should be evaluated against product stability, available access and the approved case style. A general claim that one method is always gentler or always faster is not an adequate selection basis.
Why 10 cases/minute can represent more product than 100 cartons/minute
The unit matters. Cases per minute and cartons per minute cannot be ranked as though they count the same object. First establish the number of saleable units inside each pack, then compare output for the same SKU and the same acceptance conditions.
Forester’s My Insight
Reproducible planning arithmetic—not an HIJ rating or customer result: assume one retail carton contains one bottle, and a shipping case contains 12 retail cartons. A hypothetical 10 cases/minute represents 10 × 12 = 120 retail cartons/minute. The number 10 is smaller than 100, but it describes a larger product flow than 100 of those cartons per minute.
For an order of 24,000 bottles, that pack design requires 24,000 retail cartons and 24,000 ÷ 12 = 2,000 shipping cases. Change the case count to 24 cartons and the order still requires 24,000 retail cartons, but only 1,000 cases. The case size, loading pattern and achievable rate must all be reassessed; the arithmetic does not prove that the same case packer can run the changed format.
Use this count check to prevent mismatched quotation requests. Write “12 cartons per case, one bottle per carton” instead of just “120 packs per minute.” If there are two bottles per retail carton, say so explicitly: the product quantity represented by each carton changes.
Nominal speed is not the same as accepted output. Agree the SKU, production interval, product condition and conforming-pack count used in the comparison. Detailed line rate balancing, buffers and recovery belong in the cartoning systems planning guide; they should follow the decision about which packaging levels the project actually needs.
Check whether the quotation covers loading alone or the complete package
Do not assume a case packer also erects and seals the case. An integrated arrangement can combine those functions, while another proposal may rely on separate equipment or manual work. Ask what enters the quoted equipment—flat case blanks, open cases, or products already grouped—and what leaves it.
Likewise, a cartoner quotation should identify the product-feeding arrangement, carton closure and included checks. The word “automatic” does not confirm that leaflets, code verification, rejection or every upstream transfer are included.
| Boundary | Clarification to request |
|---|---|
| Material supply | Who loads products and blanks? What must be pre-grouped or manually prepared? |
| Package formation | Which carton or case drawing is approved, and who provides any separate erecting equipment? |
| Loading and accessories | Are inserts, partitions, pads, counting and orientation changes included? |
| Closing and inspection | What closure is delivered? Which defects are checked, and what happens to a failed pack? |
| Format changes | Which SKUs and change parts are included now? Which formats require separate evaluation? |
| Delivered endpoint | Is acceptance at a retail carton, an open loaded case, or a closed shipping case? |
This scope comparison also explains why a universal “cartoner vs case packer price” is not useful. Two quotations may buy different functions, format coverage and manual-work requirements. Compare the cost of achieving the same approved output, including the equipment and tasks outside each quoted machine. Do not infer a payback period from machine price alone.
The HIJ case-packing equipment range separates the available equipment categories. Use it to identify the relevant configuration discussion, not as proof that any model includes all functions in the table.
Resolve the uncertain details with a matched sample set
Prepare the product, its retail carton if required, and its complete shipping case together. Include inserts and dividers. Mark which drawings are approved and which are still proposals. Sending a loose bottle to one supplier and a finished retail carton to another can produce different quotations even when both suppliers believe they are quoting the same project.
Review the smallest, largest and most difficult proposed formats. Relevant difficulties might include a flexible pack that changes shape, a carton that must remain upright, a visible printed surface that must not be scuffed, or a case pattern that needs an intermediate pad. These are review conditions, not automatic evidence that a machine is unsuitable.
- Confirm the count: contents per retail carton, cartons or primary packs per case, and layers per case.
- Confirm the condition: acceptable product damage, carton appearance, case squareness and closure against agreed samples.
- Confirm the handover: the orientation and support required where one machine delivers to the next.
- Confirm the exclusions: operations remaining manual, separate equipment and formats not yet evaluated.
A sample run can demonstrate the proposed loading method under the tested conditions. It does not automatically establish sustained production, every SKU or shipping performance. Keep equipment acceptance and packaging/distribution validation distinct, with responsible people and agreed evidence for each.
Choose the equipment discussion that matches your missing operation
If products still need their individual folding cartons, discuss the HIJ automatic cartoning platform and its suitability for your pack. If the retail packs already exist and need grouping into an outer case, begin with case packing. If both tasks need automation, identify the two outputs separately before specifying their connection.
The first useful inquiry is short: show the finished pack, state the contents at each packaging level, identify the operation to automate and give the required accepted output. That provides a clearer starting point than asking for a “box packing machine” without defining the box.
Not sure which packaging step you need to automate? Share the product, retail-carton and shipping-case arrangement to discuss the relevant equipment category. Compare the cartoning range with the case-packing range using the same finished-pack requirement.
Discuss My Packaging Requirement