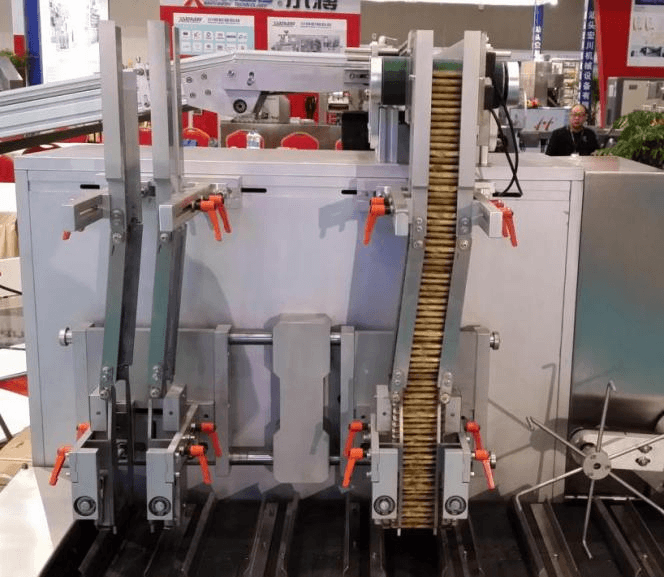
Capsule production · Inspection scope and purchasing
A capsule inspection machine checks defined characteristics and separates capsules that fail its configured criteria. Visual inspection evaluates visible features; checkweighing measures mass. Neither check alone proves the identity, potency or complete quality of the contents. Specify the defect, measurement and rejection evidence before selecting equipment.
This guide is for engineering, purchasing and quality teams planning inspection around hard-capsule filling. It helps separate machine functions and prepare a meaningful supplier test. It is not a batch-release procedure or a substitute for product-specific quality requirements.
What does a capsule inspection machine actually check?
Begin with a list of the characteristics you need to control, not a request for an “inspection machine” with no further definition. Shell appearance, capsule mass, surface powder and metal contamination are different questions. One machine may combine functions, but the proposal should identify the method and demonstrated scope of each.
| Function | Question it addresses | Do not assume |
|---|---|---|
| Visual inspection | Does the presented surface, shape, color or print meet the approved criteria? | That a camera establishes fill mass, chemical identity or unseen internal defects. |
| Checkweighing | Does the measured capsule mass fall within the agreed decision limits? | That equal total mass means equal active-ingredient content. |
| Dedusting or polishing | Has the specified surface-cleaning operation been performed? | That cleaning itself verifies appearance, mass or product identity. |
| Metal detection, where specified | Does the configured system detect the agreed metal challenge under test conditions? | That it detects every foreign material or replaces other inspection methods. |
| Reject handling | Was the identified capsule physically separated and accounted for? | That an electronic reject count proves successful removal. |
Published supplier portfolios illustrate these distinctions. Qualicaps describes visual inspection for capsule appearance defects, while Syntegon describes gravimetric capsule checkweighing. These are examples of different technologies, not evidence that the same functions are included in an HIJ filling-machine quotation.
State whether inspection is manual, camera-based or another measured process. Also distinguish sampled checks from inspection of every capsule. “All capsules pass the station” describes coverage of the population; it does not establish perfect detection of every possible defect.
Visual inspection starts with a defect library and surface coverage
Define the visual conditions that matter for your actual capsule. Candidate categories include shell cracks, dents, abnormal assembly, wrong color, stains and print defects. Whether a particular condition is detectable depends on its size, contrast, location and presentation to the inspection system. A supplier's defect list is a starting point for sample testing, not an acceptance result for your product.
Prepare controlled examples of conforming capsules and each relevant defect. Include normal variation in shell shade, print position and surface appearance so that the system is not evaluated only against an unusually uniform good sample. Have the responsible quality team agree the classification before the supplier trial.
Ask which parts of the capsule are actually viewed. A picture of the cylindrical side is not proof that both domes and the cap-body junction were examined. The handling arrangement, rotation or multiple views, lighting and image interpretation must work together. Request a demonstration of the proposed coverage using your actual capsule format.
- Size and shell family: identify the supplier, size and any elongated or special geometry.
- Appearance: identify opaque or transparent shells, color combinations, printing and acceptable variation.
- Defect position: test features at the body, cap, dome and joining region as applicable.
- Operating condition: test the agreed rate, feeding consistency and cleaning condition.
A high camera count or an “AI inspection” label does not replace these checks. Ask for demonstrated coverage, repeatable defect decisions and controlled settings for each approved capsule recipe. Keep the discussion about the required result rather than the name of the software.
Capsule weight inspection is not a direct assay of the fill
A checkweigher measures mass using its configured method. Establish whether the reported value is the gross mass of the filled capsule or a derived fill value. If a supplier claims net fill measurement, ask how shell mass is determined and associated with the result. Do not assume that a generic average shell mass removes capsule-to-capsule variation.
Simple illustration: a 600 mg filled capsule containing a 100 mg shell has 500 mg of fill. Another 600 mg filled capsule with a 110 mg shell has 490 mg of fill. The same gross reading can therefore represent different fill masses. These are hypothetical numbers, not shell specifications or permitted limits.
Nor can total fill mass alone establish formulation composition. Two blends can have the same mass and different proportions. Visual inspection and weighing should support the site's overall control strategy, not be presented as replacements for the other tests and release decisions that the product requires.
For equipment evaluation, distinguish calibration, repeatability, discrimination near a limit and actual product handling at the requested rate. Ask which reference method will be used to assign challenge values and how measurement uncertainty affects the decision. The quality and metrology teams should approve the limits and test design; no universal tolerance is proposed here.
For the capsule container and format-parts decision, use the capsule size-selection guide. Choosing the shell size and proving a weight-inspection method are connected decisions, but they are not the same task.
A detected defect is useful only if the correct capsule is removed
Evaluate the entire path from detection to separation. The system must associate the decision with the physical capsule as it moves toward the reject point. Changes in spacing, a stop or a transfer interruption can matter. Ask the supplier to demonstrate the proposed response under an approved challenge procedure.
Record where accepted capsules go, where rejected capsules go and what happens to uncertain product. A displayed counter is useful, but a count alone does not prove that the rejected items reached the intended container. Reconcile the physical challenge samples with the machine record.
| Stage | Evidence to request |
|---|---|
| Presentation | Capsules are separated and presented in the condition required by the inspection method. |
| Decision | The correct recipe and approved criteria classify each identified challenge. |
| Tracking | The decision remains associated with the intended capsule through transport and stops. |
| Separation | Rejected and accepted challenge samples are recovered from the correct destinations. |
| Fault response | The approved response to a blocked outlet, unavailable reject path or other relevant fault is demonstrated. |
| Reconciliation | Input, accepted output, rejected output and retained work in progress are accounted for. |
Do not create a challenge by defeating guards or bypassing safety devices. Agree a safe procedure with the supplier and the site's responsible team. Where a condition cannot be demonstrated at the factory, record the limitation and the evidence still required at site.
Read detection and false-reject results separately
A single overall “accuracy” percentage can hide important differences. Ask how many known defective capsules were correctly rejected, how many were missed, and how many known conforming capsules were rejected. Break the result down by defect class and test condition rather than pooling unlike challenges into one reassuring number.
Forester’s My Insight
A reproducible arithmetic example, not an acceptance criterion or HIJ test result: a hypothetical challenge contains 200 known defective capsules and 5,000 known conforming capsules. If the equipment rejects 198 defective capsules and 50 conforming capsules, the observed defect-detection rate is 198 ÷ 200 = 99%, while the observed false-reject rate is 50 ÷ 5,000 = 1%.
The reject bin contains 248 capsules, but 50 of them were classified as conforming before the trial. The accepted stream contains 4,952 capsules, including the two missed defects. Looking only at the reject count would not reveal either problem.
This calculation shows why the known status of each challenge matters. It does not make a 99% result acceptable, predict routine batch performance or prove reliability for untested defects. The test population, classification method and product risk still need review.
Preserve the sample identity and avoid counting repeated passes of the same capsule as independent evidence without explaining the design. An observed result on a small, selected challenge set should not be advertised as the detection probability for all future production.
Specify how representative samples, borderline conditions and normal good-product variation will be included. Keep detection results separate from throughput, interruption frequency and cleaning effort. A fast test with poor classification and a slow test with good classification each leave a different purchasing question unresolved.
Place inspection around the actual capsule-filling process
Map the proposed product path: filling and closing, any surface-cleaning stage, the selected inspection functions, controlled collection and downstream packaging. The exact order depends on the product and equipment. Ask which operation can introduce a defect after an earlier check and whether the final inspection point still answers the intended question.

The HIJ automatic capsule filling machine is a starting point for discussing the filling stage and its discharge requirements. Any proposed third-party inspection or weighing equipment needs a separate scope and interface review. Confirm supply responsibility, transfer method, rate, cleaning access and product accounting rather than assuming compatibility.
Do not confuse inspection of loose filled capsules with checking capsules already placed in blister cavities. At that later point, visibility and access have changed. The existing blister-machine vision inspection guide covers the packaging-stage decision.
For a multi-product line, identify recipe ownership and changeover responsibilities. The filler, inspection stage and collection arrangement must agree on the current product. A correct inspection recipe for the previous capsule format is still the wrong recipe after a product change.
Ask for a defined test, not a generic inspection guarantee
A useful request identifies the capsule supplier and size, shell appearance, fill type, required output, defect library and proposed inspection functions. Add the existing filling equipment and a simple drawing of the incoming and outgoing product conditions. State which operations are in the equipment quotation and which belong to another supplier.
Ask the proposal to identify the measurement method, included format parts, challenge procedure, reject verification, cleaning arrangements and records available to the customer. Document which questions remain open until representative samples are tested. Avoid blanket promises that the machine detects all defects or makes every batch compliant.
For the broader equipment project, compare the HIJ capsule-filling range and define the inspection boundary alongside the filling configuration. The goal is a documented control for a specific quality question, not simply an additional machine on the layout.
Planning inspection alongside capsule filling? Share your capsule format, filling process and required checks to discuss the filling-machine interface and clarify the inspection supply scope. Start with the HIJ automatic filling platform; separate inspection capabilities must be confirmed for the proposed equipment.
Discuss My Capsule Line Requirements