Capacity planning · OEE · FAT evidence
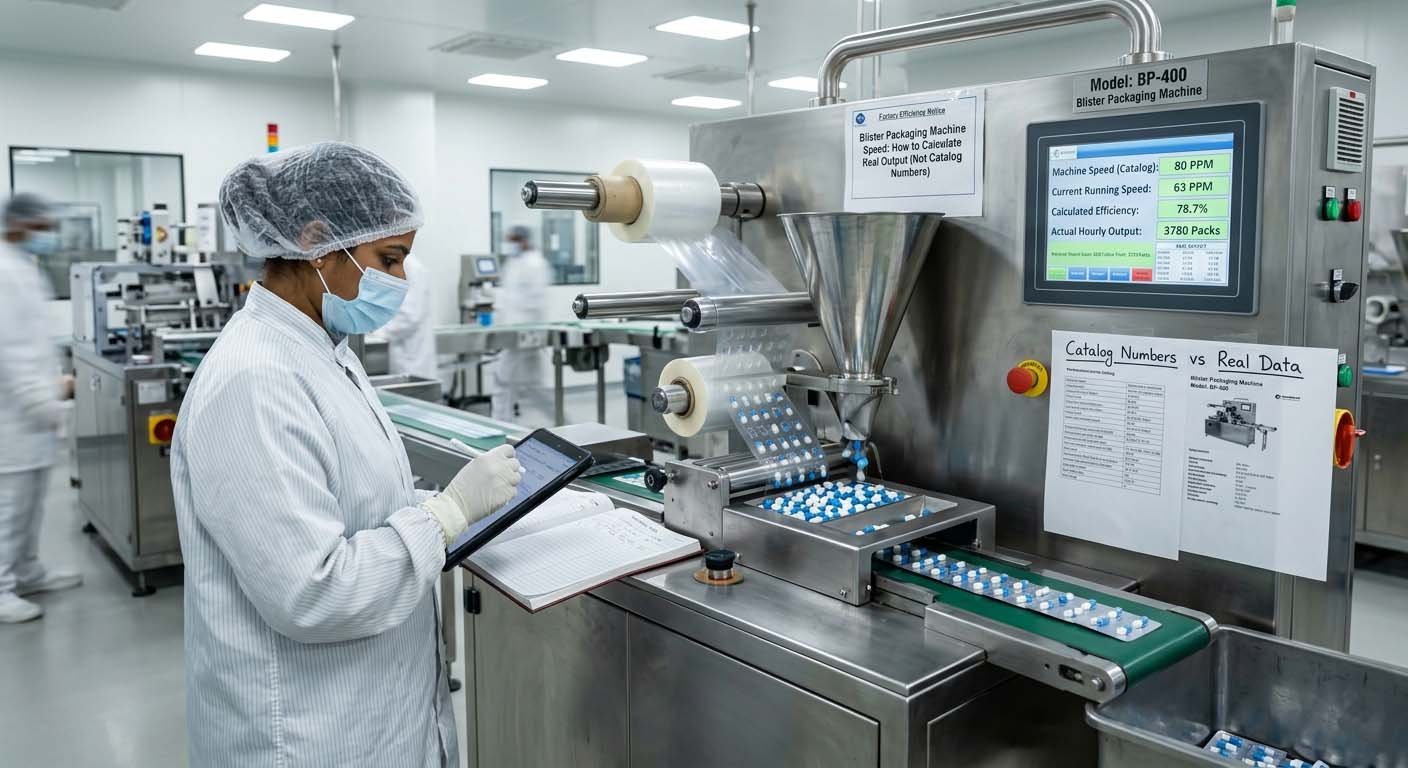
Define the counting unit before calculating output
A blister project can count cycles, cavities, product units, cut blister cards, cartons or saleable packs. These are not interchangeable. The same web index can produce several finished cards, and every card can contain several product cavities. Record the unit beside every rate before comparing machines or line proposals.
| Unit | Definition | Best use |
|---|---|---|
| Cycle or index | One repeated machine stroke or web index under the stated format. | Mechanical rate and performance calculation. |
| Blister card | One cut finished primary pack. | Primary-pack output and reconciliation. |
| Product unit | One tablet, capsule, ampoule or other item placed in a cavity. | Product accountability and feeder demand. |
| Good blister | A finished card accepted after the defined inspection and rejection process. | Usable primary-pack output. |
| Accepted carton | A completed carton with the approved blister and leaflet count. | Integrated-line and saleable-pack output. |
Calculate blister output and OEE with your verified inputs
This calculator runs only in your browser and does not save or send the values. Use data from one approved format and one defined production-time boundary. Empty fields remain uncalculated rather than being filled with assumed values.
Blister output and OEE calculator
Enter six values from the same run. Use minutes for both time inputs and blister cards for both count inputs.
Start with the ideal format rate
cycles/min × finished blister cards/cycle
Ideal product rateideal blister cards/min × product units/card
The ideal cycle rate must apply to the same product, forming web, lidding material, web width, index length, feeding method, inspection scope and downstream interface being evaluated. A cycle rate from another format is not a valid denominator for the current run.
Build OEE from availability, performance and quality
run time ÷ planned production time
Performancetotal blister cards ÷ (run time × ideal blister cards/min)
Qualityaccepted blister cards ÷ total blister cards
OEEavailability × performance × quality
Use decimals in the multiplication. The time, rate and counts must describe the same boundary. Performance above 100% usually means the ideal rate, run time, count or unit is inconsistent; investigate the inputs instead of treating the result as extra capacity.
Feeding losses belong in the recorded run
Empty cavities, product bridging, chipped tablets and repeated feeder resets may appear as performance or quality loss depending on what actually happened. Record the event first. Classify it later using a consistent site convention.
Convert OEE into accepted output
ideal blister cards/min × OEE
Good output in planned timeideal rate × planned production minutes × OEE
This result represents good output across the selected planned-production boundary. If management also needs output per paid shift, calculate that separately and label the denominator. Do not present a planned-production result and a full-shift result under the same name.
Accepted output needs an acceptance definition
Define the required seal, registration, print, coding, cavity fill and reject checks before the run. A finished card should count as good only when it meets the agreed criteria and passes the defined inspection path.
Calculate the integrated-line bottleneck
Convert every required operation to the same accepted final unit and time basis. The blister machine, inspection system, cartoner, checkweigher, case packer and manual replenishment process can each impose a different sustained limit.
good blister cards/min ÷ blister cards/carton
Sustainable line ratelowest sustained accepted rate among required operations

The lowest nominal rate is only the first screen. Buffer capacity, synchronized stops, reject handling, replenishment, recovery and changeover overlap still affect the observed shift result. Use the blister machine sizing guide to connect this calculation to annual demand, shifts and future formats.
Separate availability, performance and quality losses
| Loss category | Typical evidence | Effect on calculation |
|---|---|---|
| Availability | Breakdown, material wait, authorized intervention, unplanned cleaning or another included stop. | Run time is lower than planned production time. |
| Performance | Reduced rate, micro-stops, feeding instability or repeated reset without a logged stop. | Total count is below the ideal count for run time. |
| Quality | Empty cavities, forming defects, seal defects, coding rejects or rejected startup material inside the boundary. | Accepted count is below total count. |
When the loss record shows recurring symptoms, use the blister machine troubleshooting guide to separate forming, feeding, sealing, registration and control causes before changing the capacity assumption.
Define the FAT evidence behind the capacity claim
A quotation rate becomes useful only when the buyer and supplier can reproduce the test. Put the rate, boundary, challenge materials, stop rules and retained evidence into the FAT protocol before execution.
- Approved product or justified challenge product, forming web, lidding and printed components.
- Format drawing, finished cards per cycle, product units per card and final counting point.
- Warm-up, planned duration, replenishment, included stops and excluded time.
- Raw records for runtime, micro-stops, alarms, total count, rejects and accepted count.
- Acceptance criteria for output, defects, inspection, rejection and recovery.
- Repeatability at the agreed condition rather than one short peak-speed observation.
The blister machine FAT checklist helps turn these inputs into retained acceptance evidence.
Questions to settle before comparing proposals
- Is the quoted rate cycles, product units, blister cards or accepted cartons per minute?
- Which exact product, format and material construction produced that rate?
- Does the rate include feeding, inspection, coding, rejection and downstream transfer?
- What test duration and stop-classification convention will be used?
- Which party supplies production-representative materials and how much is required?
- Where is the final accepted count measured and how are rejects reconciled?
Compare available blister packing machine configurations only after each proposal uses the same unit, format, time boundary and acceptance definition.
Frequently asked questions
How do I calculate blister cards per minute?
Multiply the verified cycle rate for the approved format by the number of finished blister cards produced per cycle. Use cards per index from the format drawing, not cavities per blister.
How does OEE convert cycle rate into good output?
Calculate availability, performance and quality within one time boundary, multiply the three factors, then multiply the resulting OEE by the ideal blister-card rate.
What is the difference between cycle rate and blister output?
Cycle rate counts machine indexes or strokes. Blister output counts finished cards. Multiply cycles per minute by finished cards per cycle to convert between them for the approved format.
Why can OEE performance exceed 100%?
The ideal rate, runtime, count or unit is usually inconsistent. Check whether the format produces more cards per cycle, whether stopped time was excluded from runtime or whether product units were compared with blister cards.
Should changeover time be included in OEE?
It depends on the site’s approved planned-production boundary. Document the convention and apply it consistently when comparing lines, shifts or suppliers.
Should rejected startup packs count in quality?
Include them when they fall inside the selected production boundary and the site’s counting convention. If startup is excluded, document the excluded time and material separately.
What determines output on an integrated blister-cartoning line?
The slowest sustained required operation, together with buffers, synchronized stops, reject handling, replenishment and changeovers, determines accepted final output.
What should a supplier retain from a capacity FAT?
Retain the approved protocol, product and material identity, format revision, setup conditions, runtime, stop log, total and accepted counts, reject record, deviations and final approval status.
Calculation references and boundary
- OEE.com: OEE calculation, availability, performance and quality
- NIST: The Costs and Benefits of Advanced Maintenance in Manufacturing
The calculator uses the standard availability × performance × quality relationship. Your organization should approve the time model, loss categories, ideal rate and counting convention before using the result for capital approval or contractual acceptance.
Continue the capacity decision
Turn the calculation into a testable machine scope
Send your product, blister drawing, materials, target accepted output, shift pattern, inspection scope and downstream configuration. HIJ can review the inputs required for a reproducible capacity proposal and FAT.
Discuss Your Capacity Target