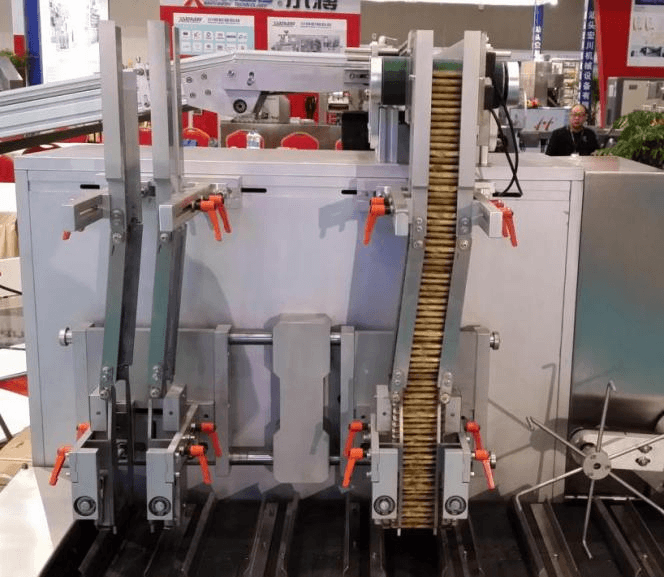
Engineering reference · component identification
The main blister packing machine parts handle the forming web, create cavities, feed the product, apply and seal the lid, transport the web, and cut and discharge the finished packs. Coding, inspection and rejection depend on the installed configuration.
Use this guide to identify a component and prepare a replacement enquiry. It covers pharmaceutical tablet and capsule blister equipment, not retail card-sealing machines. A part name describes a function; the machine-specific part number and drawing identify what to order.
Blister packing machine parts names and functions
Start with the station where the component is installed. “Roller,” “plate” or “sensor” is rarely a sufficient description because similar-looking items can appear in several locations. Record the station name before looking for an order code.
On a small screen, scroll the table sideways to read the matching details.
| Part or assembly | Main function | Record before ordering |
|---|---|---|
| Forming-web unwind | Holds and releases the base web. | Reel holder, brake or tension component, web direction and assembly reference. |
| Web guides and rollers | Guide material through its intended path. | Installed position, roller profile, bearings, surface and drawing reference. |
| Heating and forming station | Prepares and shapes the cavity. | Forming route, tool identity, cavity drawing, heater or service connections. |
| Product feeder | Places tablets or capsules into pockets. | Product dimensions, feeder type, contact parts, tracks and format reference. |
| Lidding unwind and registration | Presents the lid web to the sealing area. | Web direction, foil specification, guide arrangement and registration device. |
| Sealing station | Joins the lidding to the formed web. | Platen or roller design, seal pattern, tool revision and control components. |
| Indexing or web-transport drive | Moves material between operations. | Drive position, motion type, belt or gripper reference and interface dimensions. |
| Coding and inspection equipment | Marks or checks the pack when fitted. | Installed device model, software or format dependency and reject interface. |
| Perforating, cutting and punching tools | Produce separation lines and finished cards. | Tool set, finished-card drawing, matching die, stripper and mounting details. |
| Discharge and scrap handling | Routes finished packs and residual web. | Card orientation, guide or transfer format, conveyor and scrap-path reference. |
Station names are shared across many designs, but their mechanisms differ. For example, Uhlmann's B 1440 documentation shows alternative feeders and rotary or platen sealing. Those examples explain terminology; they do not establish compatibility with a HIJ machine.

For a new equipment project, review the HIJ thermoforming blister machine configuration. A new-machine proposal and a replacement-part enquiry require different information.
Identify the machine, assembly and individual part
Build a short identification chain: machine serial number → installed assembly → drawing item and revision → part marking. This prevents an order from being based only on a familiar model name.
- Machine identity: photograph the nameplate and record the manufacturer, model and serial number. Note relevant retrofits or previous component substitutions.
- Assembly identity: show the component in its installed location. State the station, side and position using the machine documentation's naming convention.
- Controlled reference: provide the assembly drawing number, item number, revision and existing order code where available. Keep older and current revisions clearly separated.
- Observed condition: describe what was seen or measured, when it happened and which product or pack was running. Do not turn a suspected cause into a confirmed diagnosis.
For an electrical device, photograph the complete label and connection arrangement without opening energized equipment. The supply rating alone does not identify a sensor, heater or drive. Replacement selection and installation belong with qualified personnel using the machine's technical documentation.
Separate spare parts, wear parts and change parts
Spare parts are retained or purchased to replace installed components. Wear parts are components whose condition requires periodic assessment under the maintenance plan. Change parts, also called format parts, adapt a station to a particular product, cavity layout or finished pack.
These categories overlap. A duplicate forming tool can be a spare for an existing format; a different forming tool can belong to a new format set. A worn guide may be both a wear item and a format-dependent item. Label the intended use instead of assuming each term defines a separate catalogue.
Ask whether the quote covers a single item, a matched pair, an assembly or a complete format set. A cutting punch, mating die and associated stripping parts should be identified separately where the design requires them. Do not assume a photograph of an assembly means every pictured item is included.
For the engineering of a new format, use the blister tooling and mold-design guide. This parts guide focuses on identification and replacement scope, rather than repeating the complete tooling-design workflow.
Check compatibility beyond the model name
Thermoforming and cold-forming components
Thermoforming heats a plastic forming web before shaping it. Cold forming mechanically shapes an aluminium-based laminate. Do not order a forming component from the material name or pocket count alone. Ask which forming route, tool set and machine configuration the reference belongs to.
If a machine was ordered for both routes, confirm its actual conversion scope. A forming-tool change does not by itself prove that the feeder, transport, sealing, cutting and control settings suit the proposed format.
Mechanical, material and control interfaces
- Mechanical fit: mounting, locating features, clearances, direction, matched components and service connections.
- Product and material contact: the specified material, surface and cleaning requirements for the installed location.
- Electrical or control fit: the full device reference, signals, connectors, settings and any required software or commissioning work.
- Pack-format fit: current product, cavity and card drawings, material specifications and tool-set revisions.
Uhlmann's format-parts guidance likewise treats tooling together with the machine, material and process. Its supplier-specific services are not a promise about HIJ supply or cross-brand interchangeability.
Ask the proposed supplier to state the compatibility basis and any exclusions in writing. A generic claim that a part fits “DPP machines” is less useful than an identified reference matched to the actual serial number and configuration.
Plan the checks after a replacement
Replacement is not finished when the item physically fits. Agree what must be checked after installation and who releases the machine back to production. The scope depends on the component's function and the site's approved procedures.
For a guide or transport component, checks may include alignment and controlled material movement. For a forming, sealing or cutting component, define the relevant pack measurements and acceptance checks. An inspection or reject component requires confirmation of the intended detection and rejection behavior.
Record the removed and installed references, drawing revisions, reason for replacement, work performed and results. Retain the previous component or evidence when a failure investigation remains open. Route changes to materials, geometry or controls through the applicable site review; do not assume every substitution is like-for-like.
Use the blister machine maintenance checklist for recurring maintenance planning. This article does not prescribe disassembly, electrical work, safe-isolation steps or universal replacement intervals. Follow the equipment manual and site procedures for those activities.
Prepare a replacement-parts enquiry that can be checked
A concise evidence package is more useful than a long list of possible parts. Send the machine identity, the installed location and the most specific reference available. For a missing or unreadable label, say so explicitly.
- Machine nameplate and serial number, plus relevant modifications.
- Station overview, close-up photographs and installed markings.
- Drawing and item references, revision and existing part code.
- Current product or pack format when the item is format-dependent.
- Observed condition, required quantity and destination.
- Required scope: individual part, matched items, assembly or format set.
Request confirmation of the supplied reference, included items, compatibility basis, installation requirements, availability and quotation terms. If the replacement changes the approved configuration, identify the documentation and verification work before accepting it.
Need a change-parts PDF? Request the parts list or assembly drawing for your exact machine and format. A generic download can explain names, but is not proof that its item numbers apply to your equipment. Send drawings or photos through the contact channel agreed with the supplier.
Questions about blister machine parts
What are the main parts of a blister packing machine?
Typical groups include forming-web and lidding unwinds, web guides, heating and forming equipment, a product feeder, sealing tools, web transport, coding or inspection equipment, cutting tools and discharge components. The installed parts depend on the machine design and ordered options.
Are blister machine spare parts and change parts the same?
They describe different purposes. A spare replaces an installed component, while a change part adapts the machine to a product or pack format. A spare forming tool for an existing format can belong to both categories. Confirm the item number, drawing revision and intended use.
Can the same blister machine parts fit different models?
Only when compatibility is documented. Similar names, model labels or cavity counts do not confirm matching mountings, interfaces, materials or controls. Check the machine serial number and the supplier's approved part reference before ordering.
Does an alu-alu machine use the same forming parts as a thermoforming machine?
Do not assume so. Thermoforming heats a plastic forming web, while cold forming shapes an aluminium-based laminate mechanically. A machine configured for both routes may require a defined conversion set and separate settings. Check the approved configuration and drawings.
Can a parts photograph replace a drawing or part number?
A photograph helps locate a component, but usually cannot establish its revision, internal dimensions, material or electrical specification. Combine nameplate and location photos with markings, drawings and the observed condition. Have the supplier identify an unmarked part before purchase.
Where can I get a blister packing machine change-parts PDF?
Request the machine-specific parts list, assembly drawing or format-set list from the equipment supplier. Include the serial number and current pack format. A generic PDF is useful for learning names, but should not be used as the ordering catalogue for a different machine.
Need to identify a part on a HIJ blister machine? Have the machine serial number, station photographs and available part or drawing references ready. For a complete machine project, start with the thermoforming equipment page.
Discuss a HIJ Blister Machine Part