Cosmetic equipment sourcing guide
European and Chinese cosmetic packaging machines should be compared through the same product, package, line scope and acceptance evidence. Country of origin is context—not proof of performance, compliance or lifecycle value.
What should a European versus Chinese machine comparison answer?
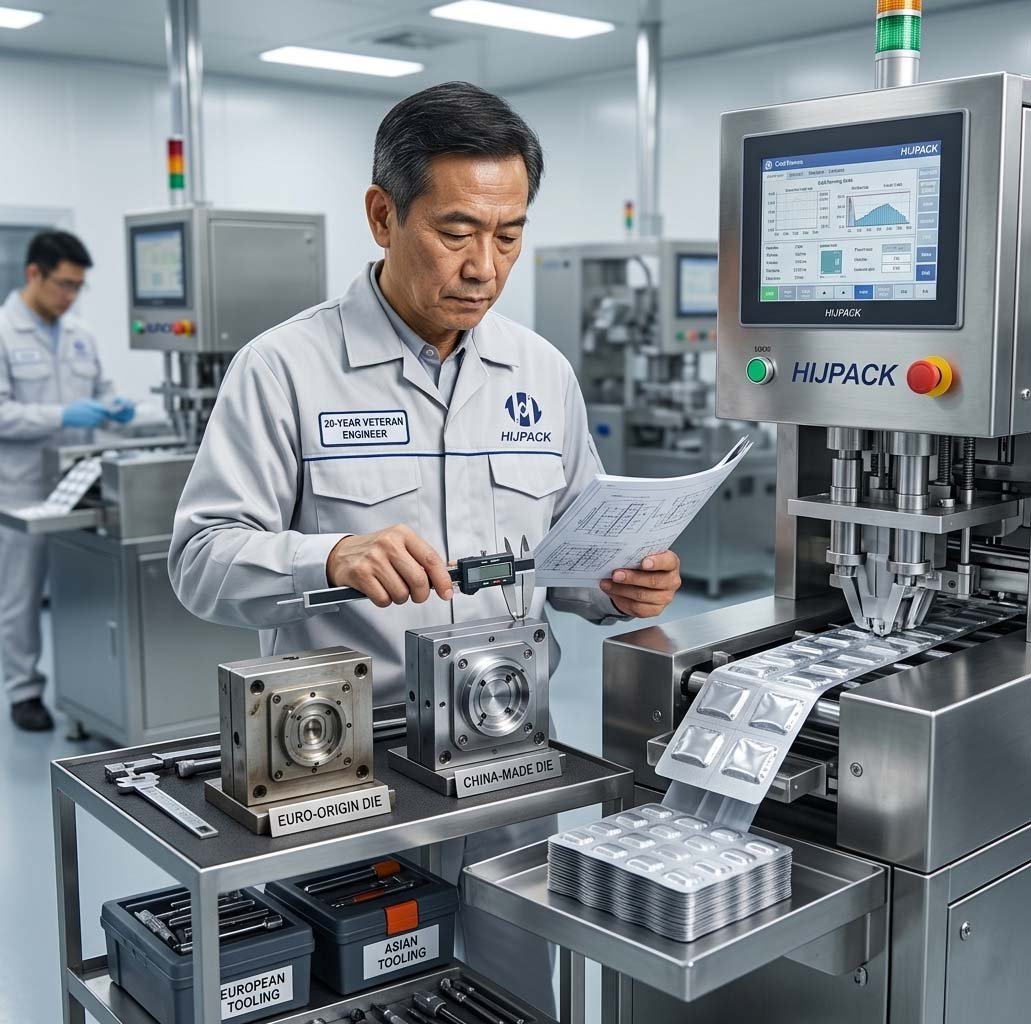
A useful comparison should answer whether a named supplier and configuration can process your product, produce the approved package, meet the accepted output target, integrate with the rest of the line and provide the evidence and support your organization requires. It should not award a result to an entire country before those inputs are known.
The correct outcome may be European, Chinese, local, hybrid or a decision to postpone purchase until the product and package are defined. The method below makes that choice auditable.
Country of origin is a weak proxy for project risk
Manufacturing location can influence logistics, language, time zones, currency and service geography. It does not directly establish fill accuracy, seal quality, cleaning access, software ownership, safety conformity or documentation completeness. Those attributes belong to a specific machine, supplier and contract.
Both regions contain suppliers with different engineering depth, product focus and support models. A comparison that uses “European” as a synonym for premium and “Chinese” as a synonym for value hides the variation that procurement must investigate.
Define the cosmetic project before comparing suppliers
A supplier cannot quote a reliable configuration from the words “cosmetic packaging line.” Cream, lotion, gel, paste, oil, powder, wipes and single-dose products behave differently. Tubes, jars, bottles, sachets and plastic ampoules require different filling and closure processes.
- Product identity, viscosity range and temperature behavior
- Foaming, stringing, dripping, particles or abrasive ingredients
- Container, closure, seal and decoration drawings
- Nominal fill and approved acceptance criteria
- SKU count, batch size and changeover frequency
- Accepted output by SKU and shift pattern
- Cleaning method and product-contact requirements
- Coding, inspection, rejection and data scope
- Upstream, downstream and facility interfaces
- Destination-market and machinery-safety requirements
Send representative product and packaging components when practical. A machine demonstrated with water and a generic container may not reproduce the behavior of the commercial product-package combination.
Normalize the scope before comparing price
Two quotations can show the same machine name while covering different work. One may include product-contact parts, change parts, guarding, coding, inspection, conveyors, electrical standards, FAT, documentation, installation and training. Another may quote only the base machine.
| Scope item | Question for every supplier | Evidence to request |
|---|---|---|
| Product path | What contacts the product and how is it drained or cleaned? | Flow diagram, material list, drawings and cleaning access review |
| Packaging formats | Which SKUs and change parts are included? | Format matrix and priced tooling list |
| Accepted output | Where is good output counted and what losses are inside the test? | Capacity calculation and FAT protocol |
| Integration | Who owns conveyors, signals, buffers, rejection and line control? | Interface specification and responsibility matrix |
| Documentation | Which documents are included, in what language and revision state? | Document index and representative samples |
| Lifecycle | What happens after shipment? | Warranty terms, escalation route, parts list and service quotation |
Use one counting unit for output
One proposal may state containers per minute, another cycles per minute and another accepted cases per hour. These values cannot be compared until they use the same finished unit, time boundary and product-package format.
Request the conditions behind every rate: product, fill, container, closure, number of lanes or heads, upstream supply, inspection, rejection and downstream transfer. Distinguish a short mechanical peak from sustained accepted output during an agreed test.
Verify filling performance with the actual product
Filling behavior depends on the product and metering principle. Accuracy or repeatability measured with one liquid does not transfer automatically to another formulation. Product temperature, entrained air, particles, bulk-tank level, nozzle behavior and line speed can change the result.
Define the measurement method, sample selection, reference equipment, acceptance limits and treatment of startup or rejected units before the test. Compare the distribution of results, not only an average that can conceal drift or individual failures.
Package quality is more than fill quantity
A cosmetic pack may also require closure torque, crimp or fold geometry, seal integrity, cap presence, code legibility, label position, cleanliness and appearance. The correct attributes depend on the package and claims, not on the supplier’s standard demonstration.
Map every critical or important attribute to an equipment control, inspection method, sampling plan and disposition rule. Do not assume that a camera proves attributes it cannot see.
Changeover evidence matters when the SKU mix is high
Quoted changeover time is meaningful only when start and finish points are defined. The boundary may include cleaning, removal, installation, adjustment, recipe selection, line clearance, verification and release—or only the mechanical exchange.
Ask suppliers to demonstrate a representative changeover with the tools, staffing and documents included in the offer. Record residual adjustments and the first accepted unit after restart. A repeatable, controlled changeover can matter more than a higher nominal rate for short batches.
Hygienic design must match the formulation and cleaning method
Product-contact material, surface condition, seals, hoses, dead legs, drainage, disassembly and access affect cleaning and contamination control. The correct design depends on formulation, cleaning chemistry, exposure time, microbiological risk and the manufacturer’s procedures.
Request product-contact drawings and a material list. Observe disassembly and reassembly. Confirm how retained product is removed and how cleaned parts are protected. Do not accept a steel grade, polish value or “GMP design” label as a substitute for the complete cleaning assessment.
ISO 22716 applies to cosmetic manufacturing practices
ISO 22716:2007 provides guidelines for the production, control, storage and shipment of cosmetic products. It is a management and manufacturing-practice framework; it is not a machine certification and it does not rank equipment by country.
Equipment suppliers can support the cosmetic manufacturer with design information, material records, manuals, cleaning access, maintenance information and test evidence. The cosmetic manufacturer remains responsible for applying its quality system and approving intended use.
FDA cosmetic guidance does not approve a machine
The FDA’s cosmetic GMP guidance and inspection checklist discusses suitable equipment design, maintenance, cleanliness and controls intended to reduce adulteration or misbranding risk. It does not grant a standalone machine approval.
If a supplier uses FDA language, ask which product classification and requirement it means. Cosmetics, drugs, medical devices and combination or dual-use facilities may have different obligations. A generic compliance badge cannot settle that scope.
EU cosmetic GMP and machinery conformity are separate questions
Regulation (EC) No 1223/2009 requires cosmetic manufacture to comply with good manufacturing practice. Machinery placed on the European market is also subject to applicable product-safety legislation. One concerns the cosmetic manufacturing system; the other concerns the machinery placed on the market.
Do not collapse both into “CE and GMP compliant.” Ask for the exact legal acts, standards, declarations, technical documents and responsibilities relevant to the supplied machine and intended use.
The EU machinery transition must be handled by delivery date
The European Commission states that machinery placed on the EU market before 20 January 2027 must comply with Machinery Directive 2006/42/EC, while Regulation (EU) 2023/1230 applies mandatorily from that date. Confirm the applicable route for the planned placing-on-market date instead of copying a declaration from another project.
The Commission’s machinery guidance also makes clear that CE marking follows the applicable conformity-assessment process. A logo or third-party “CE certificate” alone does not establish that the required work was completed.
Importers have duties when machinery comes from outside the EU
European Commission guidance states that importers must check that non-EU products meet applicable requirements and that necessary documentation is available. Therefore a Chinese supplier’s document package and the EU importer’s review must connect.
Confirm the manufacturer, importer or authorized representative roles, product identification, declaration, instructions and language needs before shipment. The Commission’s importer guidance is the starting point; project-specific legal interpretation belongs with the responsible organization and competent authority.
Controls architecture should be compared function by function
A component brand does not describe the finished control system. Compare user access, recipes, alarms, event history, audit needs, backup and restore, time synchronization, network interfaces, remote access, cybersecurity, software ownership and change control.
Ask who can modify PLC and HMI code, which files are handed over, which passwords remain vendor-controlled and how obsolete hardware will be managed. “Open” and “proprietary” need contractual definitions, not assumptions based on geography.
Line integration can erase a strong standalone result
A filler can meet its own test while the combined line stops because containers, closures, coding, inspection, conveyors or cartoning cannot sustain the same flow. Define handshake signals, stop categories, accumulation, reject tracking and restart logic for every interface.
For multi-vendor projects, name one party for each interface and one owner for overall line acceptance. For single-supplier projects, verify that subcontracted machines and third-party software are actually included in that responsibility.
Documentation should be sampled before the purchase order
A long document list is not evidence that useful documents exist. Request representative samples with confidential information removed. Check whether drawings match the offered model, protocols contain executable tests and manuals identify actual controls and maintenance points.
Technical documents
- General arrangement and utility schedule
- Product-contact and flow drawings
- Electrical and pneumatic documentation
- Software and backup inventory
Acceptance documents
- URS traceability or compliance matrix
- Risk assessment as agreed
- FAT and SAT protocols
- Deviation, punch-list and approval records
Define language, format, revision, approval route and due date. Documentation supplied after shipment has less leverage than documentation attached to contractual milestones.
Audit the factory against the offered configuration
A supplier audit should connect sales claims to engineering and manufacturing controls. Review drawing control, incoming inspection, fabrication, electrical assembly, software release, calibration, testing, nonconformance, document approval and change management as relevant to the project.
Trace one offered machine or comparable build through records. Confirm which operations are performed internally and which are subcontracted. A polished showroom does not answer those questions, and a modest factory is not automatically weak.
FAT turns claims into comparable evidence
Run the same agreed challenges for shortlisted suppliers where practical. Use representative product and components, defined operating conditions, calibrated measurement equipment and preapproved acceptance criteria.
- Confirm the test article. Record product, packaging components, format, lot and substitutes.
- Confirm the test boundary. Define warm-up, duration, replenishment, planned stops and accepted output.
- Challenge critical functions. Include filling, closure, inspection, rejection, alarms, stops and restarts as applicable.
- Record raw results. Keep counts, measurements, events, deviations and rejected units.
- Close deviations deliberately. Assign action, owner, due date, retest need and shipment effect.
Service claims need names, locations and boundaries
“Global support” and “lifetime service” are too vague for comparison. Ask where engineers and parts are located, which languages and time zones are covered, how remote access is controlled, what work is chargeable and what happens when the first contact cannot resolve the fault.
Request an escalation matrix and service quotation. If response time matters, define acknowledgement, remote diagnosis, parts dispatch and on-site attendance separately. Supplier origin alone does not predict any of them.
Build the spare-parts plan from the bill of materials
Separate consumables, wear parts, format parts, critical spares and long-lead components. Record manufacturer part numbers, alternatives, recommended quantity, storage conditions, replacement skill and replenishment route.
Ask what happens if the original component is discontinued. A credible obsolescence plan and accessible standard parts may be more valuable than an unsupported promise of fast delivery.
Total cost of ownership should use your own inputs
Do not import universal European or Chinese price ratios. Build a project-specific model from quoted and internal values: equipment, tooling, integration, factory and site tests, freight, duties, installation, utilities, training, documentation, spares, service, labor, cleaning, changeover, maintenance and expected operating losses.
| TCO input | Supplier evidence | Buyer input |
|---|---|---|
| Acquisition scope | Itemized quotation and exclusions | Tax, duty, financing and internal approval cost |
| Implementation | FAT, shipment, installation, SAT and training scope | Site work, utilities, travel and production disruption |
| Operation | Consumption, staffing and maintenance requirements | Local rates, shift model and planned utilization |
| Changeovers | Tools, staffing and demonstrated sequence | SKU plan, batch sizes and line-clearance requirements |
| Support | Parts and service terms | Inventory policy and downtime consequence |
| End of life | Upgrade, software and obsolescence path | Planning horizon and residual-value policy |
Show assumptions and ranges rather than hiding uncertainty in a single total. Recalculate all shortlisted offers over the same planning horizon.
Currency, logistics and contract terms can change the result
Quotation currency, payment milestones, exchange-rate exposure, Incoterms, freight, insurance, customs, taxes and local installation responsibilities can materially change landed cost and schedule. Compare the same delivery point and responsibility boundary.
Review title transfer, risk transfer, packing, export documents and damage inspection. Do not assume an attractive ex-works price represents an installed, accepted line.
References should be verified, not merely counted
Ask for reference projects with comparable product behavior, package, automation and region. With permission, discuss what was supplied, when it was accepted, how changes were handled and how support performed after warranty.
Do not demand confidential batch data or treat a logo wall as proof. One relevant, contactable reference can be more useful than many unrelated names.
A supplier scorecard should preserve critical gates
Weighted scores help organize tradeoffs, but a high average must not compensate for a failed safety, legal, product-quality or essential-output requirement. Identify pass/fail gates first, then score the remaining commercial and lifecycle differences.
| Evaluation area | Examples of project evidence | Decision treatment |
|---|---|---|
| Product and package fit | Trials, samples, drawings and measured results | Gate where critical |
| Machinery safety and market access | Risk assessment, declaration and technical documentation | Gate where applicable |
| Accepted output | Reproducible calculation and witnessed FAT | Gate or weighted target |
| Integration | Interface specification and responsibility matrix | Weighted with named risks |
| Documentation | Index, samples, schedule and language | Gate for required deliverables |
| Lifecycle support | Parts plan, service terms and references | Weighted over the chosen horizon |
| Commercial value | Normalized price and TCO assumptions | Weighted after technical gates pass |
Warning signs apply to suppliers in either region
- A detailed performance promise is made before product and package review.
- The quotation omits change parts, interfaces or acceptance criteria.
- Compliance is described only with logos or undefined certificates.
- The document list cannot be supported with representative samples.
- Software access, backups, licenses or remote connections are unclear.
- The supplier resists a witnessed test or will not record deviations.
- Customer references cannot be connected to a comparable application.
- Warranty and service terms use broad promises without measurable boundaries.
When should a European supplier stay on the shortlist?
Keep a European supplier when its verified configuration, application experience, local support, integration capability, documentation or lifecycle platform fits the project. An existing corporate standard or installed base can also reduce training, spares and software complexity.
These are supplier- and site-specific advantages. Confirm them in the proposal and evidence rather than treating them as automatic regional attributes.
When should a Chinese supplier stay on the shortlist?
Keep a Chinese supplier when it understands the product and package, responds with a controlled configuration, exposes scope and exclusions, accepts meaningful FAT criteria and provides an acceptable delivery, documentation and support plan.
Price can be an advantage, but it should be evaluated after required functions and evidence are aligned. Use the same technical gates you would apply to any other supplier.
A hybrid line can be valid but needs one integration owner
Some projects combine machines from different countries or specialists. This can preserve a strong process platform while using another supplier for labeling, cartoning or end-of-line equipment. It can also create interface and support gaps.
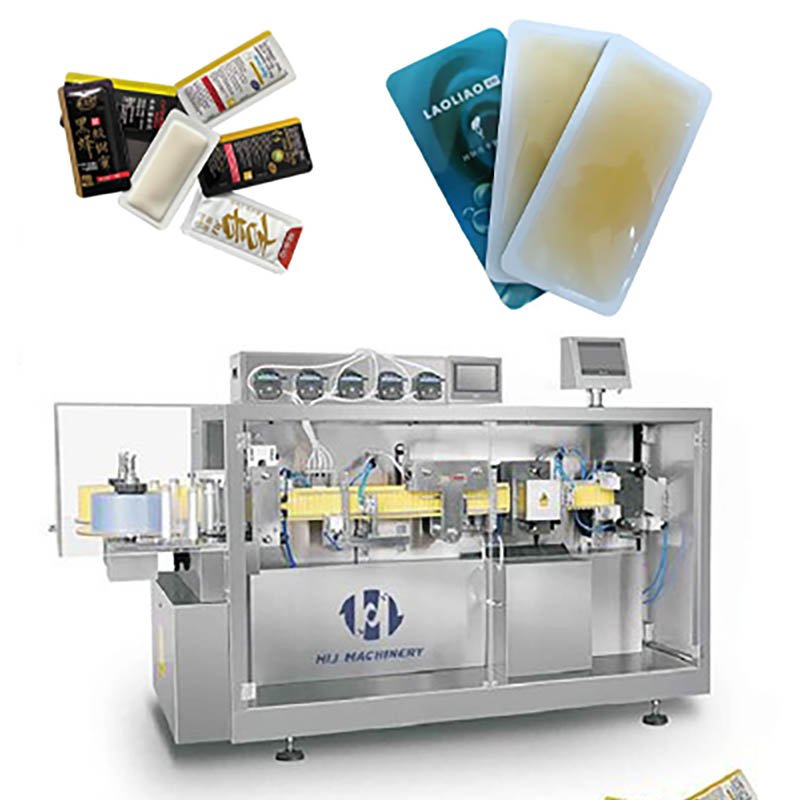
Define mechanical, electrical, control, data, guarding, validation and acceptance responsibilities at every boundary. Name the party responsible for the final accepted line rate and coordinated fault recovery.
Write the RFQ so every proposal answers the same questions
The RFQ should include product and packaging data, intended output, line layout, utilities, environment, cleaning, controls, safety, documentation, tests, delivery, installation, training, spares and support. Separate mandatory requirements from preferences.
Use the cosmetic packaging machine overview only to identify relevant equipment families. Use a project URS and supplier response matrix for the actual selection.
Put acceptance and change control into the contract
Connect payment milestones to approved drawings, document delivery, FAT, shipment readiness, SAT and punch-list closure as appropriate. Define how deviations, substitutions, software changes and schedule impacts are approved.
The contract should also identify supplied and buyer-supplied materials, test quantities, retest rules, travel responsibilities, remote-access conditions and warranty start. Ambiguity discovered during FAT is expensive; ambiguity discovered after arrival is worse.
The final decision should be reproducible
A reviewer should be able to trace the selected supplier back to requirements, evidence, risks, assumptions and approvals. Record why alternatives were rejected and which open actions remain before purchase.
Information needed for a useful supplier review
For a project-level comparison, prepare the product and container drawings, representative samples, target accepted output, SKU and batch plan, cleaning approach, line interfaces, destination market, required documents, test expectations and support location.
HIJ can then compare the requested scope with available turnkey integration and service support options. The response should identify what is confirmed, what requires a trial and what is outside scope.
Frequently asked questions
Are European cosmetic packaging machines always better than Chinese machines?
No. Country of origin does not prove project fit. Compare named suppliers and configurations using the same product, package, URS, FAT boundary, documentation scope and lifecycle requirements.
Are Chinese cosmetic packaging machines always cheaper?
No universal price ratio is reliable. Compare itemized offers at the same scope and delivery point, then include tooling, integration, tests, freight, installation, documentation, spares, service and operating assumptions in total cost.
Can a cosmetic packaging machine be ISO 22716 certified?
ISO 22716 provides GMP guidelines for cosmetic production, control, storage and shipment. It is not a universal machine-approval label. Equipment can support the manufacturer’s system through suitable design, documentation, maintenance and cleaning provisions.
Does CE marking prove that a machine is high quality?
No. CE marking concerns conformity with applicable EU requirements; it is not a quality ranking or an indication of origin. Review the applicable legislation, declaration, technical documentation and supplied configuration.
What should be tested during a cosmetic packaging machine FAT?
Use representative product and packaging components to test agreed functions such as filling, closure or sealing, coding, inspection, rejection, alarms, stops, restarts, changeover and accepted output under a documented protocol.
How should after-sales support be compared?
Compare named support locations, languages, hours, escalation steps, remote-access controls, parts stock, dispatch terms, on-site capability, exclusions and pricing. Broad promises such as global or lifetime support are not enough.
Should I buy a complete line from one supplier?
A single supplier may simplify responsibility, while specialist suppliers may provide stronger individual processes. Either model can work if every interface is specified and one party owns coordinated line acceptance and recovery.
What should I send before requesting a machine comparison?
Send product and package drawings, representative samples, fill and quality criteria, target accepted output, SKU plan, cleaning method, interfaces, destination market, documentation needs, FAT expectations and service location.
Sources and regulatory boundaries
Primary references used for the regulatory boundaries in this guide: ISO 22716:2007; FDA Good Manufacturing Practice Guidelines/Inspection Checklist for Cosmetics; Regulation (EC) No 1223/2009; European Commission machinery and CE-marking guidance. Requirements depend on the product classification, market, placing-on-market date and supplied scope. This article is a procurement framework, not a conformity assessment or legal opinion.
Compare the project evidence, not the country label
Send your product, container, accepted-output target, line interfaces, destination market and FAT expectations. HIJ will identify the proposed configuration, open tests, documentation scope and exclusions for an evidence-based comparison.