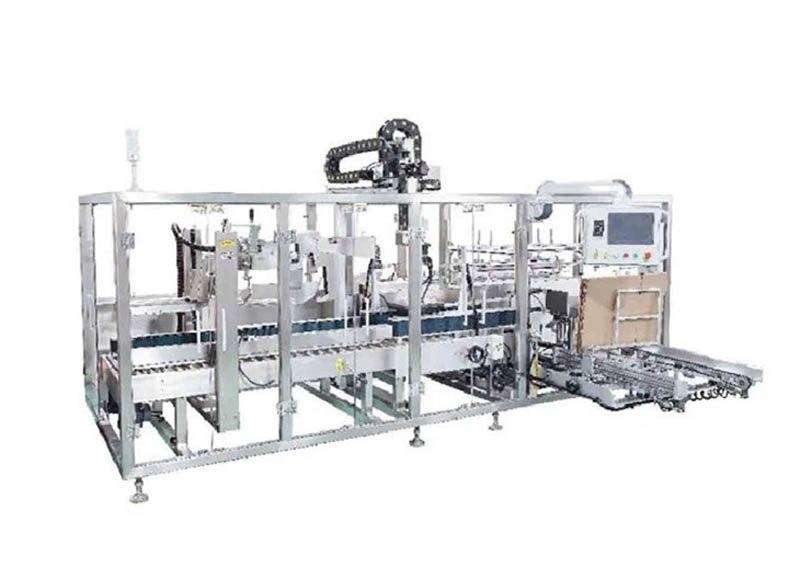
A useful blister-machine lead time is not one headline number. It is a dated, dependency-based schedule from approved inputs through design freeze, tooling, build, FAT readiness, documentation, shipment and site work.
Why a Single Lead-Time Number Is Misleading
Two suppliers can quote the same number of weeks while promising different endpoints. One may mean that the base frame is mechanically complete. Another may mean the configured machine is ready for a witnessed factory acceptance test. Neither automatically includes export preparation, freight, installation, site acceptance, qualification support or the buyer’s production release.
The starting point also matters. A schedule measured from deposit can conceal unresolved drawings, missing product samples or an unapproved URS. A more useful schedule identifies when each buyer input is due and when the supplier may legitimately stop the clock because an approval or material lot is missing.
Product, pack, materials, tooling, feeding, inspection, controls and downstream interfaces.
Approved samples, test duration, challenges, accepted output, retained records and deviation rules.
Buyer inputs, supplier work, third-party items, approvals, freight, utilities and site services.
Define the Schedule Endpoint Before Comparing Suppliers
| Milestone | What it should mean | Evidence to retain |
|---|---|---|
| Design freeze | Approved product and format matrix, pack drawing, material construction, configuration, options and interfaces. | Signed drawings, URS response, open-item list and controlled revision. |
| Mechanical completion | Specified equipment and tooling are assembled, but functional testing may still be open. | Build review, component list and outstanding-work register. |
| FAT ready | Agreed samples, utilities, instruments, software and draft protocol are ready for execution. | Readiness checklist, approved protocol and test-material identification. |
| FAT accepted | Tests are complete and deviations have an agreed disposition; this is not merely the supplier’s internal completion date. | Signed report, raw results, deviation log and approved punch list. |
| Ready to ship | Release conditions, documents, preservation, packing and export records in the contract are complete. | Release note, packing list, document index and shipping readiness record. |
| Site accepted | Installation and contracted site tests are complete under the real utility and line conditions. | SAT report, training records, open items and handover status. |
Build the Timeline Around Seven Controlled Workstreams
A project plan should show which activities can run in parallel and which are on the critical path. The sequence below is more useful than a generic day count because it exposes the information and approvals that can move the finish date.
- Application and URS review. Confirm dosage form, geometry, fragility, orientation, pack construction, output definition, inspection, data, documents, utilities and site boundary. Record every deviation and assumption.
- Samples and format definition. Receive representative products, approved drawings, forming and lidding material details, print registration information and difficult format extremes. Unverified samples keep feeding and tooling risk open.
- Design freeze and long-lead release. Approve the layout, stations, tooling, controls, component choices and interfaces before releasing project-specific work. The schedule should state how a later change affects cost and dates.
- Manufacture, software and documentation. Run frame build, tooling, control development and document preparation as coordinated workstreams. A mechanically complete machine with unfinished software or records is not FAT ready.
- Internal commissioning and FAT readiness. Prove basic functions, alarms, guarding, recipes, material handling and inspection before inviting the buyer. Identify the exact product and packaging-material lots reserved for FAT.
- FAT, deviations and release. Execute the approved protocol, retain results and samples, close or formally disposition deviations, then confirm the shipping-release boundary.
- Logistics, installation and site work. Plan export packing, freight, customs, unloading, utilities, installation, SAT, training and any contracted qualification support as separate milestones.

Inputs That Commonly Move the Critical Path
Product and material availability
A supplier cannot verify feeding, forming, sealing, registration or finished-pack acceptance from a product name alone. Confirm the quantity, lot, condition and delivery date of representative products, forming web, lidding material and printed samples. If commercial material cannot be supplied, document the substitute and the retest required later.
Tooling and change parts
Each cavity layout, web width, seal pattern, perforation, cut geometry and feeder route can create project-specific work. Freeze the complete format list before comparing schedules. Add late formats through a controlled change rather than pretending they fit the original date.
Controls, inspection and line interfaces
Recipes, coding, vision, reject confirmation, audit trails and upstream or downstream signals require functional definitions and test cases. Component brand approval is not enough; the schedule must include programming, integration, challenge testing and retained evidence.
Buyer review and third parties
Drawing approval, artwork, serialization vendors, validation reviewers, freight forwarders and site contractors may sit outside the machine supplier’s direct control. Put their required dates and owners in the same schedule. Otherwise a supplier promise can appear late when the real unresolved dependency belongs elsewhere.
How to Verify a Promised Blister Machine Lead Time
Ask every candidate supplier for the same deliverables before awarding the purchase order. A credible answer should make assumptions visible rather than hide them inside one attractive date.
- Dated milestone plan: design freeze, drawing approval, tooling release, internal test, FAT readiness, FAT, document completion and ready-to-ship dates.
- Responsibility matrix: each product, sample, drawing, approval, third-party interface, utility and site action has an owner and due date.
- Configuration baseline: named stations, options, formats, controls and approved components—not only a machine model.
- Change-control rule: explains how late product, artwork, material, scope or component changes affect price and schedule.
- FAT readiness criteria: defines protocol approval, sample quantities, material lots, instruments, test duration and prerequisites.
- Document index: states which manuals, drawings, certificates, backups and qualification-support documents are supplied, in what format and by which milestone.
- Deviation and punch-list process: distinguishes a critical release blocker from an item that may remain open under an approved plan.
- Shipping and site boundary: separates factory release from transport, customs, unloading, installation, SAT, training and buyer qualification.
FAT and Qualification Documents Must Have Their Own Schedule
EU GMP Annex 15 describes qualification and validation as lifecycle activities based on justified, documented risk assessment. It also notes that equipment may be evaluated at the vendor before delivery and that tests performed during FAT may not need to be repeated at site when transport or installation does not affect the tested function and the decision is justified. The buyer still owns the site qualification and validation strategy.
This means “documentation included” is too vague. Name the URS response, approved drawings, risk information, FAT protocol, raw results, deviation records, manuals, calibration evidence, software or parameter backups and any IQ/OQ support expected from the supplier. Assign draft, review and final-delivery milestones instead of postponing the entire document package until shipment.

How Buyers Can Shorten the Schedule Without Hiding Risk
- Send a controlled product and format matrix with representative samples before requesting the final schedule.
- Resolve pack drawing, material construction and print registration before tooling release.
- Approve standard components or named alternatives early, including the process for substitution.
- Review drawings and protocols within agreed response windows and appoint one authorized decision owner.
- Run documentation, site preparation and logistics planning in parallel with machine manufacture.
- Use remote design reviews and FAT witnessing when appropriate, but keep objective acceptance evidence.
- Freeze additions after design approval; route genuine changes through their own cost and schedule impact.
Schedule compression should come from earlier decisions, parallel work and faster approvals—not from removing the tests or records needed to accept the configured machine.
Compare Quotations on the Same Timeline Boundary
| Comparison field | Question to ask | Evidence required |
|---|---|---|
| Start condition | Does the clock start at deposit, approved URS, samples received or design freeze? | Dated prerequisites and owner list. |
| Configuration | Which formats, feeder, inspection, coding, data and line interfaces are included? | Controlled scope and approved drawings. |
| FAT endpoint | Is the date internal completion, FAT readiness or buyer-accepted FAT? | Approved protocol and release criteria. |
| Documents | Which drafts and final records are due before FAT and before shipment? | Document index with dates, format and approval status. |
| Logistics | Are packing, inland transport, freight, insurance, customs or unloading included? | Incoterm, route assumptions and responsibility matrix. |
| Site completion | Who installs, commissions, trains and supports SAT or qualification? | Site plan, prerequisites, duration and handover evidence. |
Red Flags in a Lead-Time Proposal
- The supplier quotes one date before reviewing the product, pack drawing, material and format matrix.
- The proposal uses “standard documentation” without a document index, revision, language or delivery milestone.
- FAT is described as a machine demonstration instead of an approved protocol with acceptance criteria and retained results.
- Buyer approvals and sample-delivery dates are absent, so the supplier can later redefine the cause of delay.
- Tooling, feeding, inspection or software is “to be confirmed” while the headline date remains unchanged.
- Ready to ship is presented as production ready, with freight, utilities, installation, SAT and qualification left unplanned.
What to Send for a Useful Schedule and Quotation
Send enough information for the supplier to expose—not guess—the critical path:
- Product form, dimensions, weight, fragility, orientation, feeding behavior and representative samples.
- Finished blister drawing, cavity layout, forming web, lidding material, print and registration details.
- All planned formats and the difficult minimum and maximum conditions.
- Accepted finished packs per minute or shift, planned run duration, reject treatment and data required.
- Coding, inspection, rejection, recipe, audit-trail and line-interface requirements.
- URS, document index, FAT expectations, site-support boundary, destination utilities and target production window.
For the equipment route, review the blister packing machine selection hub. To define acceptance evidence, use the blister machine FAT checklist.
Continue the Procurement Decision
Frequently Asked Questions
How long does a blister packaging machine from China take to deliver?
When should the lead-time clock start?
What is the difference between FAT ready and ready to ship?
Does quoted lead time usually include ocean freight and installation?
Which buyer inputs can delay a blister machine project?
How should two suppliers’ lead times be compared?
Can FAT evidence support site qualification?
What should I send HIJ for a project schedule?
Regulatory and Technical References
- European Commission, EU GMP Annex 15: Qualification and Validation.
- ICH Q9 Quality Risk Management guideline.
- FDA, Process Validation: General Principles and Practices.
Build a Defensible Blister Machine Schedule
Send your product, pack, material, format and FAT requirements. HIJ can return a project-specific configuration boundary, open-input list and milestone structure for quotation review.
Discuss My Project Schedule