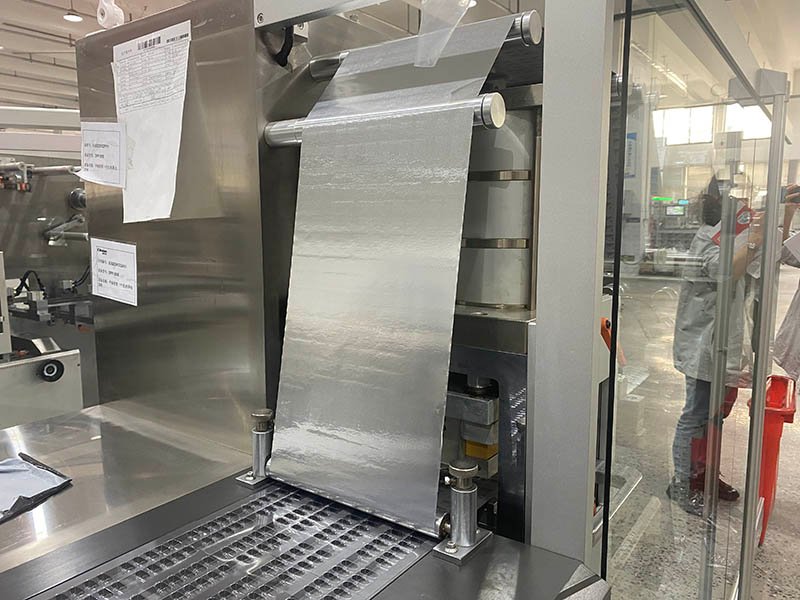
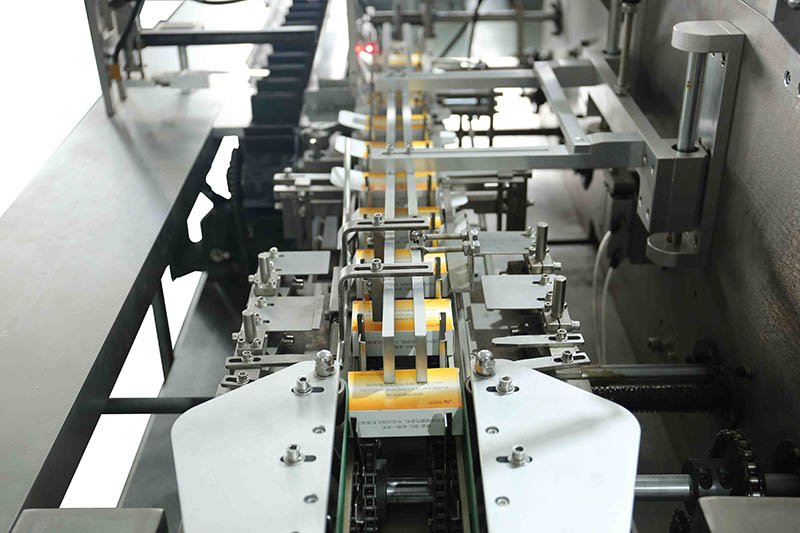
Troubleshoot a bottle cartoning machine by station and evidence. Protect people and product first, capture the alarm and rejected sample, identify the last correct step, then change one verified variable at a time.
This guide covers bottle infeed, carton pick and erection, leaflet handling, product insertion, closure, coding and discharge. Exact limits, energy-isolation steps, adjustment points and replacement procedures must come from the applicable machine manual and the site’s approved procedures.
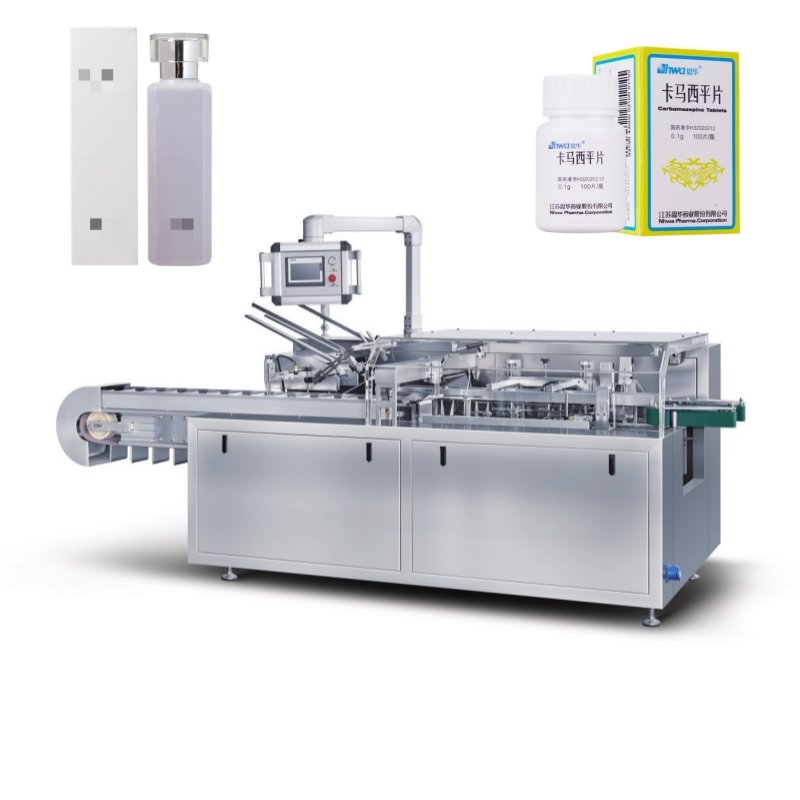
What should you do when a bottle cartoner faults?
Do not begin by turning several setpoints or repeatedly resetting an overload. Record the machine state first: alarm text and time, active recipe, product and packaging-material lots, station position, rejected sample, upstream and downstream status, and the last adjustment. This evidence separates an isolated event from a repeating pattern.
If inspection, unjamming, cleaning, adjustment or repair could expose anyone to unexpected movement, electrical energy, compressed air, stored mechanical force or hot surfaces, follow the site’s energy-control procedure and the machine manual. OSHA’s control-of-hazardous-energy standard establishes minimum requirements for isolating hazardous energy during covered servicing and maintenance; local legal requirements may differ.
Only trained and authorized personnel should enter guarded areas, defeat an interlock, access electrical panels or work on stored-energy systems. Never use this article as a substitute for the site lockout/tagout procedure, risk assessment or model-specific manual.
Quick diagnostic sequence: make the condition safe → preserve the alarm and sample → find the last station that completed its action correctly → compare the failed input with the approved sample or recipe → change one permitted variable → run a controlled confirmation and record the result.
Use a five-step troubleshooting method
Define the symptom
Name what is observable: a missing bottle, unopened carton, skewed leaflet, damaged label, unlocked flap, unreadable code or repeated stop at a named station.
Preserve the evidence
Save the alarm, affected carton, bottle and leaflet, recipe/version, material lot, time, speed condition and operator action before clearing the event.
Locate the last good step
Work upstream from the visible defect. Confirm whether the bottle arrived, the carton opened, the leaflet transferred, insertion aligned and closure completed.
Test one cause
Compare against drawings, approved samples and the manual. Make one authorized correction so its effect can be distinguished from other variables.
Confirm and retain
Run enough material to show the condition is stable, inspect accepted and rejected packs, then record the action and any open follow-up.
If an operator changes guide width, conveyor speed and sensor position together, a successful restart does not reveal which change solved the problem—and an unsuccessful restart creates three new unknowns.
Station map: where the evidence points
| Observed symptom | Check first | Evidence to retain |
|---|---|---|
| Bottle tips or gaps | Actual bottle dimensions and stability, guide continuity, transfer points, accumulation and upstream delivery. | Bottle sample, video of the transfer, recipe and event time. |
| Carton not picked | Blank condition, magazine presentation, vacuum status, cup condition and carton-presence detection. | Blank lot, failed blank, alarm and vacuum/air observation allowed by the manual. |
| Carton opens poorly | Creases, squareness, board condition, pick timing, erection tooling and change-part identity. | Flat and erected samples, carton drawing and tooling revision. |
| Leaflet absent or skewed | Leaflet specification, stack condition, separator/pick action, fold path, sensor cleanliness and detection logic. | Leaflet lot, folded sample, reject reason and challenge result. |
| Bottle or carton damaged | Bottle-to-carton clearance, insertion alignment, pusher timing, carton support and product presentation. | Matched bottle/carton samples, damage location and slow-cycle observation where permitted. |
| Flap or glue failure | Carton geometry, closing-tool alignment, adhesive specification, application condition and compression path. | Closed sample, material lot, settings record and agreed closure test. |
| Code unreadable | Device status, approved message, print/emboss location, surface condition and verification settings. | Sample, message version, inspection result and rejected code image. |
| Repeated overload | Stop location, debris or obstruction, tooling identity, lubrication/maintenance status and drive condition. | Alarm history, location, sample, last change and authorized inspection result. |
Twelve common fault patterns
Each entry below is a diagnostic starting point, not a universal cause. The actual mechanism and permitted correction depend on the machine configuration, controls, guarding, product and approved changeover settings.
Zone 1: bottle infeed and accumulation
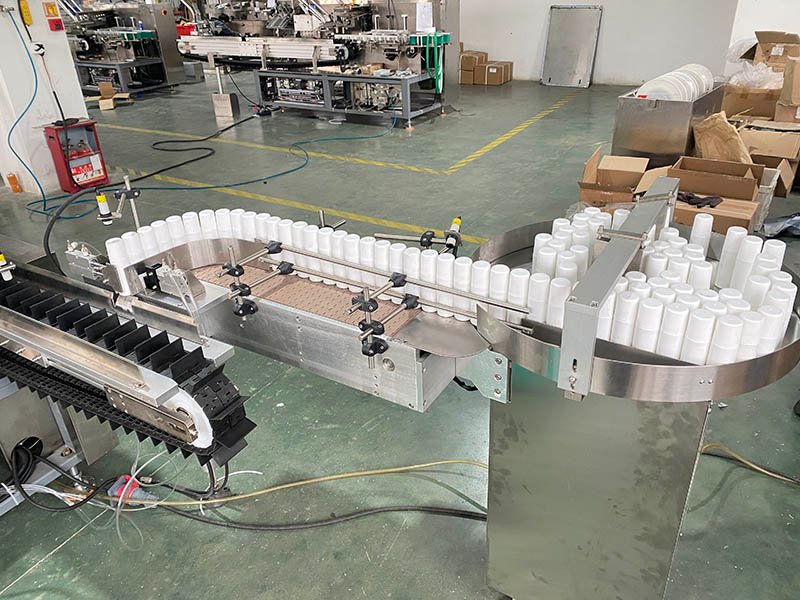
1. Bottles tip or jam before transfer
Evidence: tipping begins at the same rail joint, curve or speed transition; scuff marks may identify the contact point.
Check: actual bottle/cap geometry, center of gravity, guide continuity, pocket/change-part identity and upstream presentation. Compare with the approved format drawing and recipe before making an authorized adjustment.
2. The cartoner pauses with no internal jam
Evidence: the bottle-ready condition is absent when the machine waits; upstream equipment shows micro-stops or insufficient accumulation.
Check: line-state signals, bottle availability, buffer recovery and stop logic. Do not increase cartoner speed before proving that the upstream line can supply the required accepted rate.
3. Bottle count or orientation is wrong
Evidence: an incorrect group reaches the loading point or the inspection system flags a repeatable orientation defect.
Check: feeder setup, product-specific change parts, sensor challenge, recipe selection and manual replenishment method. Retain both the failed group and the correct reference sample.
Zone 2: carton pick and erection
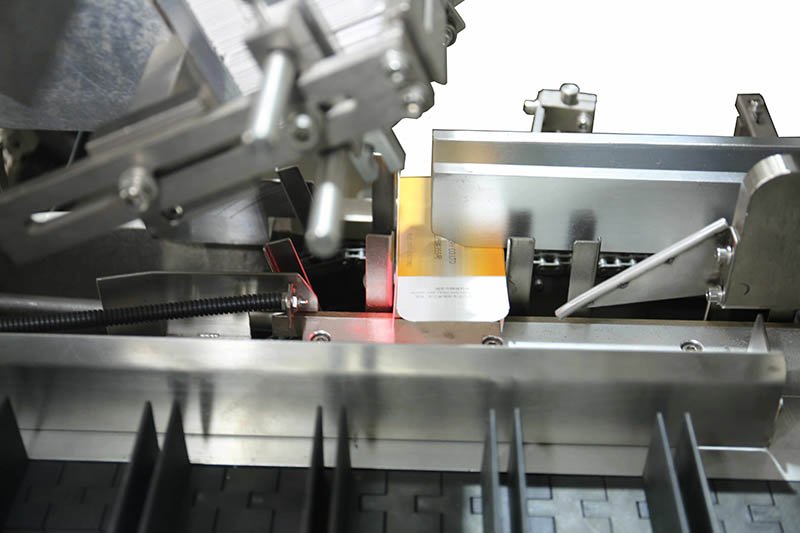
4. A carton blank is not picked
Evidence: no blank leaves the magazine, or the blank releases before reaching the erection position.
Check: blank presentation, vacuum indication, cup condition, line/filter condition where accessible, carton sensor and magazine setup. Replace or adjust only under the approved maintenance procedure.
5. Two cartons are picked together
Evidence: nested blanks reach the opening station, often associated with one material lot or magazine refill.
Check: blank separation, static, surface finish, stack condition and separator settings against the manual. Compare another approved carton lot before concluding that the machine is at fault.
6. The carton opens skewed or collapses
Evidence: the same crease or panel fails, or the erected carton is out of square before loading.
Check: carton drawing, crease quality, board condition, erection-tool alignment, cup contact and timing. Hand-opening an isolated blank can help reveal a material problem, but machine acceptance still needs a controlled run.
Zone 3: leaflet handling and insertion
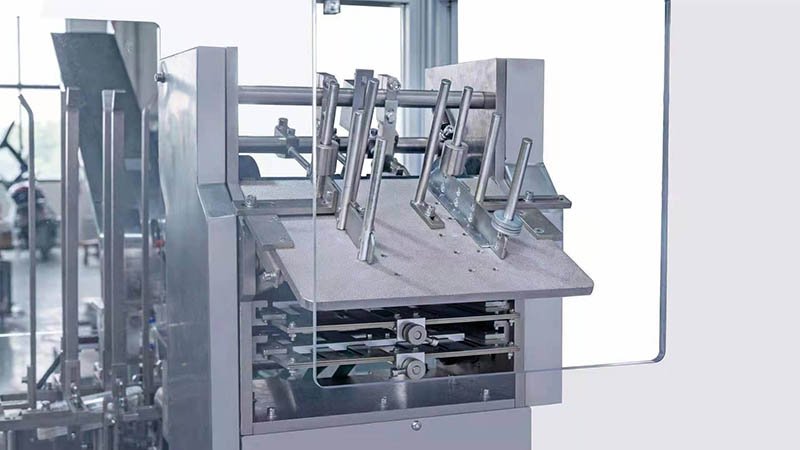
7. Leaflets fold skewed or jam
Evidence: the fold drifts in a consistent direction, residue appears on the path, or a new leaflet lot changes behavior.
Check: leaflet size, paper and fold specification; stack condition; approved roller/path setup; cleanliness; and change-part identity. Do not invent a roller gap—use the documented format setting.
8. Missing-leaflet rejects increase
Evidence: inspect the rejected cartons to separate a true missing leaflet from a false detection.
Check: pick/transfer action, vacuum status where applicable, sensor cleanliness and alignment, detection challenge and reject confirmation. Never disable the quality check simply to keep the machine running.
9. Bottle or carton is damaged during insertion
Evidence: marks repeat at the same location on the bottle, label or carton; the damage may vary by material lot or format.
Check: actual bottle and carton dimensions, guide and pusher alignment, carton support, insertion timing and approved clearance. Use jog or reduced-speed observation only when allowed by the machine’s safe operating procedure.
Zone 4: closing, coding and discharge

10. Tuck-in flaps do not remain closed
Evidence: identify which flap or tongue fails and whether the blank closes correctly by hand.
Check: carton cut/crease/slot geometry, closing-tool identity and alignment, guide condition and downstream disturbance. A carton-material nonconformance cannot be corrected reliably by forcing the machine setting.
11. Hot-melt closure is weak, excessive or stringing
Evidence: record adhesive product, lot, application condition, pattern, substrate and closure-test result.
Check: the adhesive supplier’s specified operating window, heated-system status, nozzle condition, pattern position and compression path. Hot surfaces and stored pressure require the applicable safety and maintenance procedure.
12. Code failure or repeated overload stop
Code evidence: retain the carton, approved message and inspection result; distinguish message, print quality, position and verifier faults.
Overload evidence: retain the exact stop location and alarm history. If it repeats after the permitted basic checks, stop resetting it and escalate to authorized maintenance or the supplier.
Separate material, machine and line-interface causes
A useful investigation assigns the failure to the smallest defensible boundary. Carton creases, board condition, leaflet curl, bottle dimensions and label friction belong to the incoming-material and product boundary. Vacuum generation, tooling alignment, sensors, drives and closing mechanisms belong to the machine boundary. Starvation, blocking, buffer length, interlocks and signal timing belong to the line-interface boundary.
The same symptom can cross boundaries. A missed carton may result from a damaged cup, a vacuum restriction, nested blanks, a wrong magazine setting or a carton-presence sensor. Use a controlled comparison—such as another approved material lot or a retained reference sample—before replacing parts or changing a validated recipe.
| Boundary | Questions to answer | Corrective evidence |
|---|---|---|
| Product/material | Did dimensions, lot, supplier, storage, coating, crease, label or leaflet condition change? | Incoming records, drawings, retained samples and lot comparison. |
| Format/changeover | Are the correct parts, recipe, positions and checks installed for this SKU? | Tooling IDs, recipe revision, setup checklist and first accepted sample. |
| Machine | Is there wear, contamination, misalignment, sensor drift, pneumatic loss or a repeatable drive alarm? | Alarm history, inspection record, approved measurements and replaced-part ID. |
| Line interface | Is the cartoner starved, blocked or receiving the wrong ready/fault/reset signals? | Event timeline, buffer level, I/O status and upstream/downstream alarm records. |
| Procedure/training | Was the approved setup, replenishment, cleaning, restart and line-clearance method followed? | Operator log, training status, checklist and deviation record. |
Build a fault log that reveals repeat causes
A short structured log is more useful than a long narrative. Record the timestamp, SKU, material lots, recipe, operating condition, alarm, station, rejected sample ID, immediate action, confirmation result and escalation owner. Use the same fault names so events can be counted without merging different problems into “machine stopped.”
Review faults by SKU, material lot, station and time since changeover or maintenance. Repetition after one specific carton batch suggests a different investigation from repetition after every format change. The log also improves remote support because the supplier receives a reproducible sequence rather than a general complaint.
- Photograph or export the alarm before reset when permitted.
- Keep the failed bottle, carton and leaflet together with their lot identities.
- Record the last known good pack and the first failed pack.
- Name every adjustment and who authorized it.
- State how many consecutive acceptable packs confirmed recovery.
- Link repeated failures to corrective action and closure evidence.
Preventive maintenance should follow the manual and risk
Universal “daily, weekly and monthly” times are not reliable across all cartoners. The correct interval depends on the model, duty cycle, environment, carton dust, adhesive system, pneumatic quality, product, safety functions and supplier instructions. Build the site schedule from the equipment manual, risk assessment, maintenance history and observed wear.
Typical categories include inspection and cleaning of approved surfaces and sensors; condition checks for vacuum components, guides and wear parts; lubrication at named points with the specified material; verification of guards, interlocks and reject functions; review of pneumatic and electrical alarms; and backup or control of recipes and software where applicable. Do not lubricate, clean or adjust moving equipment outside the approved safe procedure.
Choose spares from the installed bill of materials
Do not copy a generic internet spares list into a purchase order. Start with the installed bill of materials and the supplier’s recommended spares. Rank items by wear rate, failure consequence, lead time, local availability and whether replacement requires supplier support. Record exact part numbers and revisions; brand names alone do not prove interchangeability.
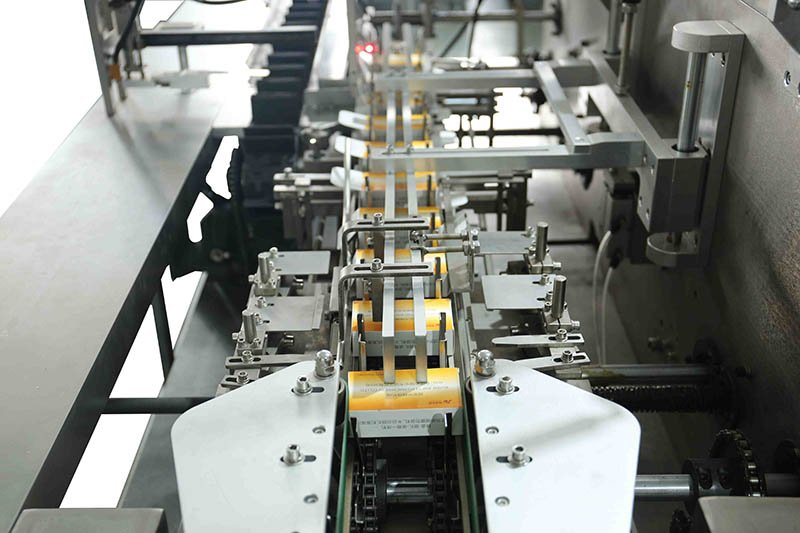
Design troubleshooting out during FAT
The best time to define fault evidence is before shipment. The URS and FAT protocol should identify which alarm appears for each challenge, how the line stops, what the operator sees, which product or carton is rejected, whether rejection is confirmed and what data is retained. Test realistic material and interface conditions rather than only an ideal demonstration.
For the published HIJ-130B bottle cartoning platform, the product page states that the final bottle feeder, leaflet, coding, inspection, line-interface scope and accepted output must be confirmed against the approved product, materials and URS. The same principle applies to troubleshooting: only installed and tested functions should be assumed available.
| FAT challenge | Expected definition | Record to retain |
|---|---|---|
| No bottle / wrong group | Machine and line response, alarm, carton handling and reject behavior. | Challenge result, sample and event record. |
| No carton / failed pick | Stop or prevention logic and safe operator recovery sequence. | Alarm, recovery steps and confirmation run. |
| Missing leaflet | Detection boundary, carton response, rejection and reject confirmation. | Challenge identity and retained reject result. |
| Wrong or unreadable code | Device/vision response and disposition of affected cartons. | Message version, failed image/sample and result. |
| Upstream/downstream stop | Starved/blocked behavior, buffer recovery and signal exchange. | I/O state, timeline and restarted accepted output. |
| Guard or overload event | Defined safe stop, alarm location and authorized reset conditions. | Safety-test record and approvals. |
When should the issue be escalated?
Escalate whenever safety is uncertain, an interlock or guard is involved, the same overload or drive fault repeats, electrical or control work exceeds the site’s authorization, a validated setting would need to change, the root cause remains unknown, or accepted product quality cannot be assured. Quarantine affected product according to the quality system when its status is uncertain.
A useful support request contains a short video from outside the guarded area, machine/model and serial identification, alarm text and history, SKU and recipe, product/carton/leaflet lots, photos of the failed sample, last change or maintenance action, and the checks already completed. HIJ’s service and support page identifies remote video troubleshooting as an available support route; response scope and timing should be confirmed for the individual project.
Send evidence, not only “the machine stopped”
Share the machine model, alarm, fault station, SKU, material lots, rejected sample and a safe video of the sequence. HIJ can review whether the next step belongs to material, format setup, line integration, maintenance or supplier service.
Request a Cartoner Fault ReviewFrequently asked questions
Why does a bottle cartoning machine keep stopping without an internal jam?
The cartoner may be waiting for a bottle-ready or downstream-ready condition rather than suffering an internal fault. Check the line-state signals, bottle accumulation and upstream/downstream event history. Confirm the cause from the HMI and I/O evidence before changing machine settings.
What should be checked first when cartons do not open?
Retain the failed blank and check carton presentation, crease and board condition, vacuum status, cup condition, carton detection, erection-tool identity and recipe/setup against the approved drawing and manual. A material-lot comparison can separate carton variability from a machine condition.
How do I distinguish a missing leaflet from a sensor fault?
Inspect the rejected carton and retain the leaflet and event record. If the leaflet is absent, review pick and transfer. If it is present, review the approved sensor challenge, cleanliness, alignment and detection logic. Do not bypass the inspection function to reduce rejects.
Why are bottles or cartons damaged during insertion?
Possible boundaries include actual product/carton dimensions, guide or pusher alignment, carton support, format-part identity and insertion timing. The location and repeatability of the damage help narrow the cause. Use only the model’s approved safe observation and adjustment procedure.
What information should be recorded for a repeated cartoner fault?
Record time, SKU, recipe/version, product and material lots, alarm text, station, rejected sample, upstream/downstream state, last change, action taken, authorization and the confirmation result. Consistent names allow recurring faults to be analyzed by station, SKU and lot.
Can operators clear every bottle cartoner jam themselves?
No. Site authorization, the risk assessment, energy-control procedure and machine manual determine who may perform each task. Any exposure to unexpected movement, stored energy, electrical systems, hot surfaces or defeated guarding requires the applicable safe-isolation and maintenance controls.
How often should a bottle cartoning machine be maintained?
Use the model-specific manual, duty cycle, environment, risk assessment and maintenance history. Generic daily, weekly or monthly times cannot replace the installed equipment schedule. Adjust intervals through an approved maintenance process using recorded condition and failure evidence.
When should I contact the cartoning machine supplier?
Escalate when safety is uncertain, an interlock or guard is involved, a drive or overload fault repeats, the required work exceeds site authorization, a validated setting may need to change, the root cause remains unknown or affected product quality cannot be assured.
Continue with bottle cartoning decisions
Sources and scope
- HIJ Automatic Bottle Cartoning Machine — published HIJ-130B planning data, configuration boundary and FAT basis.
- HIJ Service & Support — current supplier support routes, including remote video troubleshooting.
- OSHA 29 CFR 1910.147, Control of Hazardous Energy — hazardous-energy control requirements for covered servicing and maintenance.
This guide supports structured diagnosis; it is not a repair manual or safety procedure. Follow the installed machine documentation, approved recipes, site quality system, risk assessment and applicable legal requirements.