Pharmaceutical blister packaging comparison
Alu-Alu and PVC/Alu describe two different blister package constructions. Alu-Alu uses an opaque cold-form laminate for the cavity; PVC/Alu uses a transparent PVC-based thermoforming web with aluminum lidding. The right choice comes from the drug product, proposed market pack, stability evidence, user needs and the complete converting process—not from one generic barrier number.
This guide compares what packaging, quality, engineering and procurement teams must decide: material identity, protection, visibility, cavity geometry, sealing, inspection, equipment configuration, testing, output and lifecycle cost.
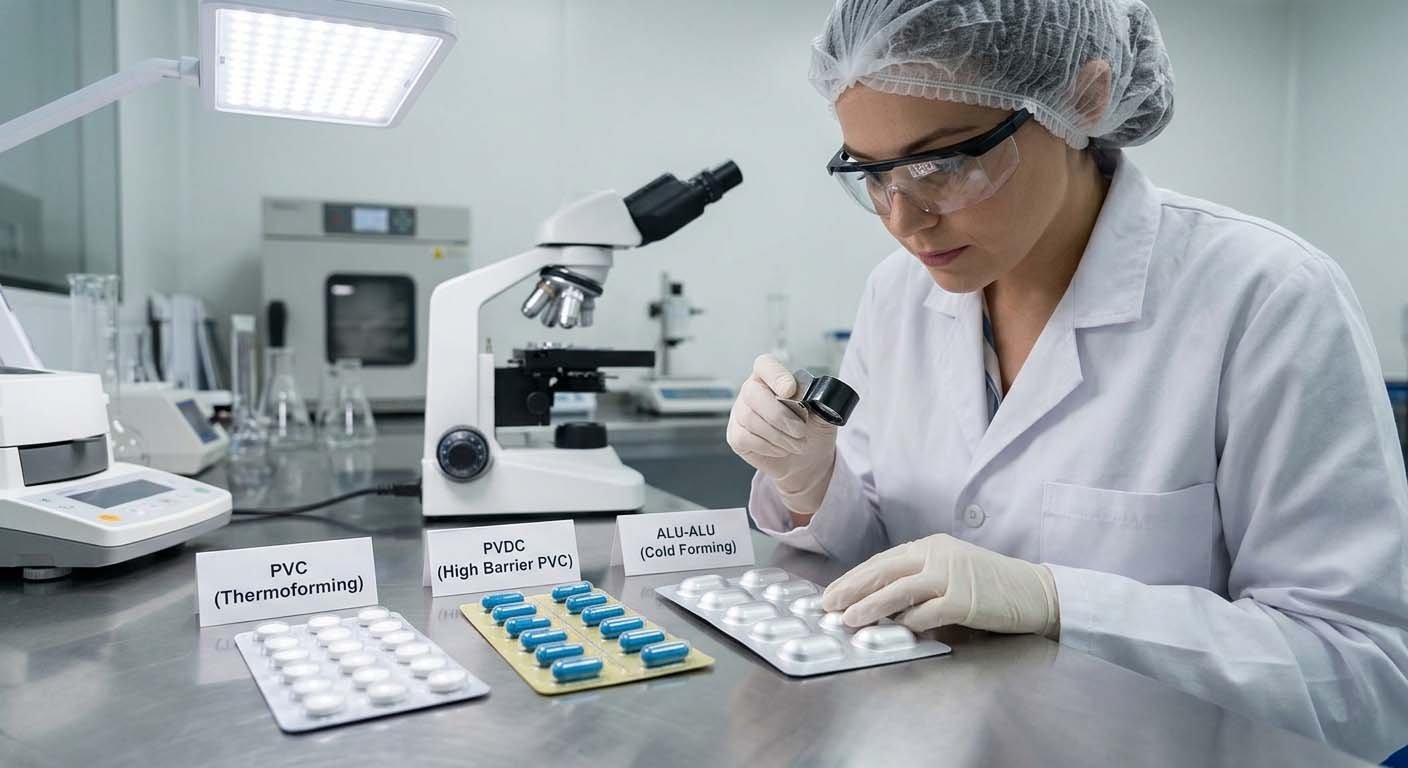
Decision boundary: this article is a selection framework, not a product-specific packaging approval. The drug manufacturer must establish suitability using the exact product, forming web, lidding, blister design, manufacturing process, storage claim and applicable regulatory programme.
Direct answer
What is the difference between Alu-Alu and PVC/Alu blister packaging?
The comparison is not “aluminum versus plastic.” Both formats normally use an aluminum lidding component; the main difference is the forming web and how the cavity is created. That difference changes material behavior, tool design, cavity footprint, inspection options, line configuration and commercial performance.
Do not start by asking which material is universally best. Start by defining what the product must be protected from, how long and under which proposed storage and distribution conditions. Then compare candidate market packs using aligned supplier data, formed-package tests and stability results.
Terminology
Define the complete package before comparing it
“PVC/Alu” is convenient shorthand, but it can hide important differences. The transparent forming web may be uncoated rigid PVC, a coated PVC structure such as PVC/PVDC, or another approved PVC-based construction. Thickness, coating weight, supplier grade, colour and forming behavior can all affect the package and process. The aluminum lidding also has a defined alloy, temper, thickness, heat-seal coating, primer and print system.
“Alu-Alu” is also a family name rather than a complete specification. A cold-form laminate contains functional layers selected for forming, barrier, mechanical support and sealing compatibility. Its exact construction, total thickness, forming direction and supplier tolerances matter. Two materials sold under the same broad label should not be assumed interchangeable.
For every comparison, record the forming web supplier and grade, full declared structure, nominal thickness, width and applicable tolerances; the lidding supplier, grade and seal coating; and the approved blister drawing. This converts a broad material discussion into a package-system decision.
At-a-glance comparison
Alu-Alu vs. PVC/Alu decision table
| Decision factor | Alu-Alu cold-form blister | PVC/Alu thermoformed blister |
|---|---|---|
| Forming web | Opaque multilayer cold-form laminate containing aluminum. | Transparent PVC or defined PVC-based thermoforming structure. |
| Lidding | Compatible lidding structure, commonly aluminum-based for push-through packs. | Compatible aluminum lidding foil for the defined pack. |
| Forming route | Mechanical cold forming without heating the web to thermoform it. | Controlled heating followed by plug, pressure, vacuum or combined thermoforming, depending on equipment. |
| Barrier position | Usually selected for a stronger moisture, oxygen and light barrier position when correctly formed and sealed. | Depends strongly on web grade and any barrier coating or laminate; transparent visibility is retained. |
| Product visibility | No visual inspection through the opaque forming web. | Product can normally be seen through the transparent cavity. |
| Cavity footprint | Often larger because laminate forming limits influence corner radii, draw depth and flange geometry. | Often more compact because a heated polymer web can conform to tighter geometry, subject to material limits. |
| Machine requirement | Cold-form station, matched tooling, suitable web handling and compatible downstream modules. | Thermoforming station, heating control, matched tooling and cooling appropriate to the web. |
| Evidence needed | Exact laminate data, forming study, seal/integrity results, stability evidence and production qualification. | Exact film/coating data, thermoforming study, seal/integrity results, stability evidence and production qualification. |
| Cost question | Evaluate material, larger card or carton effects, machine configuration, output and avoided product risk. | Evaluate selected barrier grade, material use, line efficiency, inspection value and stability suitability. |
The table describes common engineering differences, not universal performance limits. A converter’s data and the approved package specification control the actual comparison. If a third option such as PVC/PVDC is relevant, use the broader blister packaging materials guide to compare material families before narrowing the final two candidates.
Package construction
Alu-Alu forms an opaque cavity from a cold-form laminate
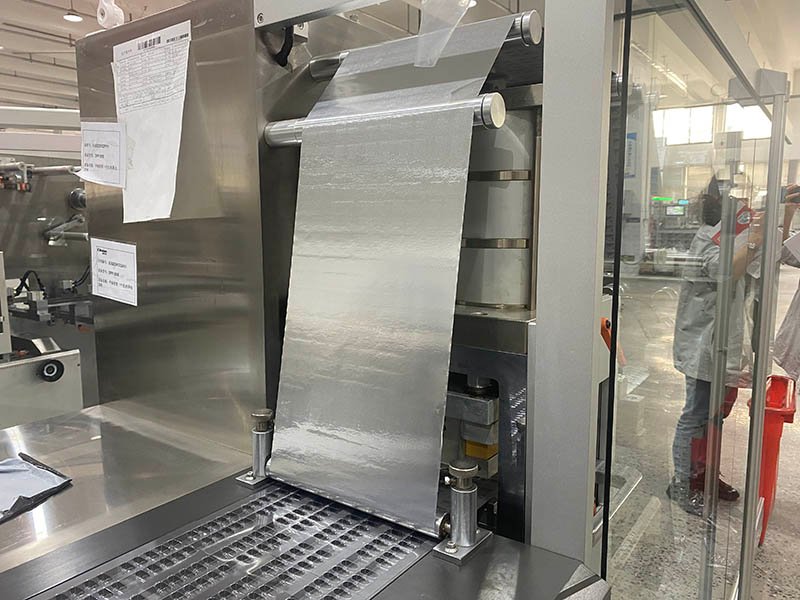
The Alu-Alu forming web is mechanically pressed into a shaped cavity at or near room temperature rather than softened in a heating station. Its aluminum-containing layer supports the high-barrier position, while polymer layers contribute sealing compatibility and mechanical protection. The exact layer arrangement must come from the material supplier’s current documentation.
Cold forming stretches and bends the laminate around the tooling. The draw ratio, corner radii, cavity depth, forming direction and tooling clearance determine how strain is distributed. Excessive local strain can cause thinning, pinholes, delamination or cosmetic defects even when a flat material sample has strong barrier data. The formed cavity, not the unused roll, is the relevant package component.
Opaque cavities also alter inspection strategy. Operators and cameras cannot confirm product presence by looking through the forming web after sealing. Inspection may need to occur before lidding, with controlled tracking from detection to the final cut and reject point.
Package construction
PVC/Alu thermoforms a transparent PVC-based cavity
For PVC/Alu, the forming web is heated within a defined operating window and drawn into cavities. Tool temperature, heating time, pressure or vacuum, plug assistance, cooling, web tension and material thickness influence cavity shape and thickness distribution. A stable process protects the flange used for sealing and keeps cavity position aligned with feeding, printing and cutting.
Uncoated PVC provides a baseline transparent structure. Coated or laminated PVC-based webs may be considered when a stronger barrier position is required without losing product visibility. Their forming and sealing behavior can differ from uncoated PVC, so “PVC compatible” on a machine brochure does not qualify every coated grade.
The aluminum lidding closes the cavity after product feeding. Calling the final pack PVC/Alu therefore describes both sides of the package but still omits supplier grade, thickness, coating and heat-seal requirements. Those details belong in drawings, material specifications, batch records and qualification protocols.
Protection
Compare barrier data only under aligned test conditions
Water-vapour transmission rate and oxygen transmission rate are often used to compare flexible barrier materials. A lower reported value can indicate a stronger barrier only when the test method, temperature, humidity or pressure conditions, units, sample structure, conditioning and orientation are comparable. Copying values from unrelated supplier brochures can create a false ranking.
ASTM F1249 addresses water-vapour transmission through flexible barrier materials, including multilayer and coated structures, and cautions that relationships involving thickness and water-vapour pressure should be used carefully. That is one reason not to convert a generic film value into a finished-blister shelf-life claim.
Request the current technical data sheet, certificate of analysis or conformance, test report and acceptance specification for each exact candidate. Record the method and conditions beside every number. If data are not aligned, treat the comparison as directional and commission suitable testing rather than calculating unsupported equivalence.
Finished package
Flat-film data do not prove formed-blister performance
A blister package includes the formed cavity, lidding, seal and all effects introduced during converting. Cavity walls may thin during thermoforming. Cold-form laminate may experience high strain at corners. Seal contamination, wrinkles, channels, web misregistration, tool damage or cutting defects can create failure paths that are absent from a laboratory film specimen.
Build an evidence ladder. Begin with supplier material data to screen candidates. Next, form production-intent cavities and inspect dimensional and visual results. Seal them with the intended lidding and process window. Apply appropriate package tests with defined sensitivity and acceptance criteria. Finally, generate the stability evidence required for the proposed market pack.
Do not let one test answer every question. Seal strength measures the force needed to separate a defined seal specimen; it does not by itself prove leak tightness, barrier or shelf life. A leak method detects defects within its method capability; it does not characterize chemical compatibility. The test set should map to identified product and package risks.
Stability
Let the proposed market pack and stability programme decide protection
ICH Q1A(R2) explains that stability testing provides evidence of how product quality changes with time under environmental influences such as temperature, humidity and light, and supports shelf life and storage conditions. For drug products, the stability studies use the dosage form packaged in the container closure system proposed for marketing.
This means a material-family comparison cannot independently approve the pack. The programme must use the exact or scientifically justified representative product, cavity construction, lidding, seal process and presentation. Target markets, labeled storage conditions and distribution risks also belong in the strategy.
A stronger nominal barrier may reduce one exposure risk, but the total suitability assessment also includes compatibility, protection, safety and performance of the packaging system. FDA container-closure guidance emphasizes product-specific evaluation. A package accepted for one formulation or strength should not be copied to another without an approved assessment.
Climate and markets
Do not turn climatic zones into a universal Alu-Alu rule
Humidity and temperature conditions matter to stability planning, but a destination country does not automatically select a single blister material. The product’s degradation pathway, proposed shelf life, storage statement, distribution route, pack count, secondary packaging and candidate package performance all affect the decision.
Statements such as “Alu-Alu is required for every tropical market” are too broad. A PVC-based barrier structure may be supported for one product, while another product may need a stronger package even in a less severe distribution environment. The evidence is the approved stability programme and market-specific regulatory strategy, not a slogan.
When multiple markets are planned, define the commercial presentations early. One global high-barrier pack may simplify supply but increase material and carton use. Market-specific packs may optimize cost but add SKUs, artwork, validation, inventory and changeover complexity. Compare the complete operating model before deciding.
Visibility
Product visibility changes inspection and patient experience
A transparent PVC-based cavity lets operators, cameras, pharmacists and users see the dosage form from the cavity side. That can support presence, colour, shape and gross-defect inspection where lighting, presentation and validated vision capability are suitable. Visibility can also help users identify whether a cavity has already been emptied.
An Alu-Alu cavity is opaque. Product inspection must generally occur before the lidding blocks the view, or use another justified method. The line must maintain the relationship between an inspected cavity position and the final card through sealing, indexing, cutting and rejection. Test that tracking during stops, restarts and reject events.
Visibility is not automatically superior. Light-sensitive products may benefit from an opaque package, while some patient or market presentations value transparency. Human-factors and artwork teams should review opening sequence, cavity identification, dose information and residual-product visibility along with technical protection.
Format engineering
Cavity geometry can change card and carton size
Cold-form laminate needs generous geometry to distribute forming strain. Compared with a thermoformed cavity for the same tablet or capsule, the cold-form design may need broader shoulders, larger corner radii, shallower drawing strategies or more flange area. That can enlarge the blister card or reduce the number of products per card within the same web width.
The effect continues downstream. A larger card can change cartoner buckets, leaflet and carton dimensions, bundle patterns, shipper cases, pallet count and distribution volume. It can also change print area, perforation location and patient opening behavior. A material-price comparison that ignores package geometry is incomplete.
Freeze the product orientation and cavity drawing before approving tooling. Review maximum local draw, formed-wall appearance, flange flatness, seal land, cutting clearance and card stiffness. Produce samples with production-intent material and confirm fit through the complete packaging and cartoning route.
Process route
Cold forming and thermoforming need different machine functions
Thermoforming uses controlled heat and a forming mechanism suited to the selected polymer web. Cold forming uses matched male and female tooling or another defined mechanical system to press the laminate into shape. The material path, forming force, index, tool alignment and web guidance therefore differ.
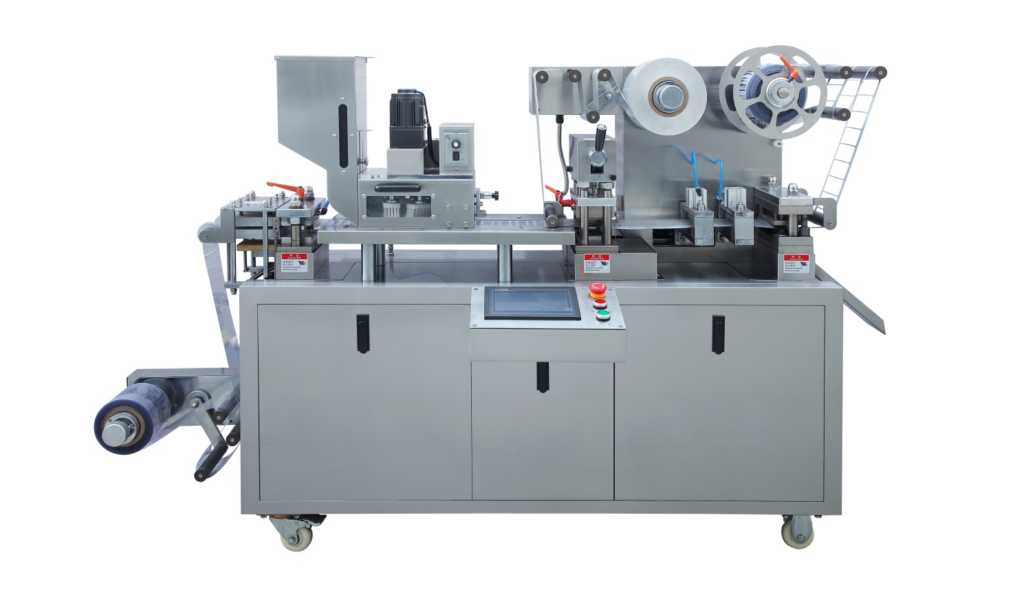
Some blister machine platforms can be configured to support both routes, but that statement is only a starting point. Confirm the exact model, installed modules, permissible web width, index range, tool envelope, material path, feeding location, seal area, coding, cutting and downstream transfer. Conversion may require more than exchanging one forming tool.
The detailed process distinction belongs to the thermoforming vs. cold-forming guide. This page keeps the focus on choosing between the two finished package concepts and translating that choice into a controlled equipment project.
Product handling
Feeding must match both the product and the cavity presentation
A material change can alter cavity pitch, orientation, pocket depth, line rate and the distance between forming and sealing. Those changes affect feeder design even when the tablet or capsule is unchanged. Product fragility, dust, static, surface friction and dimensional variation also determine whether brush, channel, track, pick-and-place or another feeding concept is suitable.
Define acceptable empty cavities, doubles, misplaced products, chipped tablets, opened capsules, scuffing and contamination of the seal land. Separate prevention by the feeder from detection by an inspection system. A camera may reject certain defects but does not make an unstable or damaging feed process acceptable.
Trials should include representative product lots, normal hopper levels, replenishment, planned operating range, stops and restarts. Record interventions rather than excluding them from the result. A package format that protects the product but cannot be filled reproducibly is not a complete commercial solution.
Sealing
The lidding and seal process must be qualified as a system
Both pack types require a lidding material compatible with the forming web and the intended opening method. Heat-seal coating, seal temperature, pressure or force, contact time, machine rate, web tension, tool flatness and seal-land cleanliness influence the result. Cold-form and PVC-based webs may require different windows.
Define the seal requirement from product and package risk. Visual appearance, seal strength, leak performance, opening force and evidence of channels or wrinkles answer different questions. Use named methods, calibrated equipment, sample conditioning, locations and acceptance criteria. ASTM F88/F88M covers measurement of seal strength in flexible barrier materials and identifies specimen failure mode, but a project still needs its own justified limits.
Include start-up, steady operation, planned stops and restart. Material held at a heated sealing station during a stop may need removal or special disposition. Verify the procedure and the machine’s index tracking so affected packs do not enter accepted production.
Materials compatibility
Check contact, migration and sealing compatibility
Barrier is only one aspect of suitability. Packaging components can interact with the product through sorption, leachables, extractables, permeation or chemical incompatibility. Printing inks, primers, coatings, adhesives and recycled or reworked material policies may also matter to the application and market.
Request current supplier declarations and technical documentation for every component, then have packaging development, quality and regulatory personnel determine what testing is required. Maintain traceability from the approved structure to received material lots. A supplier change, layer change, coating change or manufacturing-site change may require formal impact assessment.
Sealing compatibility must be demonstrated with both web components and the production process. An aluminum lidding grade that seals successfully to one PVC coating should not be assumed suitable for a different coating or cold-form seal layer. Control the complete material pairing in the specification and change-control system.
Printing and coding
Plan artwork, codes and registration with the material choice
Opaque Alu-Alu offers printable surfaces but eliminates the visual product window. Transparent PVC/Alu can present the product through the cavity while placing fixed and variable information on lidding or secondary packaging. The layout must preserve seal areas, opening paths, registration marks, codes and inspection zones.
Define preprinted artwork ownership, roll-winding direction, repeat length, registration tolerance, variable information, print technology, code verification and reject response. If the forming web is printed, forming strain can distort graphics. If lidding is printed, web stretch, tension and repeat control can affect alignment with the cavities and cuts.
Line clearance, material identification and reconciliation procedures remain necessary regardless of automation. The blister packaging printing guide provides the detailed URS and inspection boundary for artwork and variable data.
Opening and use
Evaluate push-through, peel and child-resistant functions
Many solid-dose blisters use push-through aluminum lidding, but the required opening mode depends on the product, patient population and market. Peelable, peel-push and child-resistant structures change lidding, sealing, scoring, package dimensions and test requirements. Do not assume the same lidding specification serves every market presentation.
Cavity stiffness and opacity influence use. A transparent cavity can show the tablet position before pressure is applied. An opaque cold-form cavity may need stronger graphic or tactile cues. Deep or large cavities may change the force path and how easily the product exits without damage.
Define opening performance and any child-resistant or senior-friendly requirements with the responsible packaging and regulatory teams. Use applicable standards and representative users where required. Machine acceptance should confirm that the converted pack is consistent enough for the separately approved functional evaluation.
Capacity
Compare accepted output, not catalog cycles
A machine cycle rate does not equal accepted blister cards per minute. Packs per index, cavity layout, feeding stability, forming and sealing dwell, inspection, coding, cutting, reject events, replenishment, roll changes and downstream stops determine usable output. Cold-form geometry can also reduce packs across a given web width.
State the comparison basis: product, material supplier and grade, blister drawing, lidding, tooling, inspection scope, line boundary, scheduled test time and which stops are included. Count accepted packs at the agreed output point and record rejects, waste, stops and operator interventions.
A slower nominal cycle can produce a better business result if the line is stable and the package meets shelf-life needs. A faster thermoforming route is not valuable if it fails the protection requirement. Conversely, a high-barrier cold-form concept is not valuable if its enlarged card and unstable feed make the proposed presentation impractical. Use one total system model.
Changeover
Tooling and format strategy affect lifecycle flexibility
Changing between PVC/Alu and Alu-Alu may involve the forming module, tools, heaters or cold-form mechanisms, guides, feeder parts, seal parameters, inspection recipes, printers, cutting tools and downstream parts. The exact work depends on the selected machine platform and formats.
List every intended product-material-format combination in a matrix. Identify shared and dedicated parts, storage, lifting aids, cleaning, setup checks, recipe control and first-off approval. Define the changeover start and finish so supplier estimates can be compared on the same basis.
If only one format will run for years, dual-process flexibility may have little value. If the portfolio changes frequently, a platform designed and qualified for both routes may reduce future project risk. Purchase flexibility only when supported by realistic products, drawings and operating plans; generic “future-proof” capability can add cost without a controlled use case.
Waste and yield
Measure material use per accepted dose or pack
Roll price is an incomplete cost metric. Calculate forming and lidding area per card, cards per dose, web trim, start-up loss, splices, roll-end loss, in-process rejects, inspection samples and scrap from stops or changeovers. If cold-form geometry enlarges the card, include the increased lidding and downstream carton material.
Record waste during representative sustained trials. Separate unavoidable design trim from process loss and quality rejects. A lower-cost web can become expensive if the forming window is narrow, rolls track poorly or seals are unstable. A higher-cost material can be justified when it supports product stability, but the assumption should be tested rather than asserted.
Also define segregation, reconciliation and disposal of printed or product-containing waste. Opaque material can make visual reconciliation harder, while transparent material may simplify some checks. Site procedures and applicable environmental requirements determine the final handling route.
Facility impact
Utilities, footprint and environment belong in the comparison
Thermoforming requires controlled heating and often cooling or heat removal. Cold forming requires suitable mechanical force and tooling. Both routes need electrical supply, compressed air or other utilities according to the exact configuration, as well as space for rolls, change parts, access, maintenance and material handling.
Room temperature and humidity can affect materials, products, feeding, static and sealing. Define environmental operating ranges at the machine boundary and confirm them during trials and qualification. Do not treat facility HVAC as a substitute for package protection unless the complete storage and distribution strategy supports that conclusion.
Review machine width and length together with the card and cartoning consequences. A compact blister machine may still create a larger downstream footprint when the selected format increases carton size or needs additional inspection and accumulation. Confirm the entire line layout, operator routes, material flow and maintenance clearance.
Equipment selection
Confirm exact machine configuration before approving the package

A product page or platform name does not prove compatibility with the proposed pack. Send the supplier the product drawing and samples, complete forming and lidding specifications, blister drawing, output requirement, inspection and coding scope, downstream interface and qualification expectations.
Ask the supplier to identify the proposed forming method, installed modules, web and index envelope, format-part list, feeding concept, seal control, inspection and rejection sequence, printer and cartoner interfaces, utilities and exclusions. Mark every assumption and deviation before approving the design.
If the project is evaluating an Alu-Alu configuration, review the Alu-Alu blister packing machine application page as a platform reference, then confirm the exact quoted configuration. Use the blister packing machine URS guide to convert the selected package into testable procurement requirements.
Commercial model
Calculate total cost instead of declaring one format cheaper
PVC/Alu often begins with a lower material and conversion burden than cold-form Alu-Alu, but the final comparison depends on the exact PVC-based barrier grade, package size, supplier, volumes, equipment and product risk. Alu-Alu can carry higher material and footprint costs while supporting a stronger protection strategy where the evidence requires it.
Build the cost model from forming and lidding material per accepted card; secondary packaging and distribution volume; machine and tooling investment; accepted output; labor; utilities; waste; changeover; inspection; qualification; inventory and SKU complexity. Include the cost and schedule impact of stability work for each candidate.
Risk should be explicit rather than converted into a dramatic unsourced loss claim. Record the consequence of inadequate protection, delayed launch, package change, complaint or recall using the manufacturer’s approved business and quality methods. The decision can then balance evidence, probability and impact without pretending one universal return-on-investment figure applies.
Selection workflow
Choose between Alu-Alu and PVC/Alu in seven controlled steps
Document rejected candidates and the reason. That history supports future changes and prevents the project from repeating unsupported assumptions. If a material, supplier, cavity or process changes, route the change through the quality system and assess what development, stability and qualification evidence must be repeated.
Decision matrix
Use weighted criteria only after defining pass/fail requirements
A scoring matrix can help compare acceptable candidates, but it must not average away a critical failure. First define non-negotiable requirements such as stability suitability, compatibility, approved opening performance, legal artwork, equipment feasibility and package integrity. Remove or redesign any candidate that cannot meet them.
| Criterion | Question | Evidence owner |
|---|---|---|
| Product protection | Does the proposed market pack support quality through the claimed shelf life and storage conditions? | Packaging development, stability, quality and regulatory. |
| Pack performance | Do formed cavities, seals and opening functions meet approved criteria? | Packaging development and quality. |
| Patient and market use | Does visibility, artwork, opening and dose presentation suit intended users and markets? | Human factors, regulatory and commercial teams. |
| Process capability | Can the configured line form, feed, seal, inspect, code and cut repeatably? | Engineering, production and quality. |
| Capacity | Does sustained accepted output meet the production plan? | Operations and industrial engineering. |
| Lifecycle cost | What is the total cost per accepted pack, including downstream and change impacts? | Procurement, finance and operations. |
| Supply resilience | Are specifications, change notification, lead times and qualified sources adequate? | Supply chain and quality. |
Weight the remaining criteria according to the project, cite the evidence used for each score and record uncertainty. A transparent decision trail is more useful than a highly precise score built from generic assumptions.
URS
Give machine suppliers a project-specific input package

- product type, drawing, dimensions, tolerances, orientation, fragility, dust, static and representative samples;
- forming web and lidding supplier, grade, complete structure, thickness, width, winding and technical data;
- approved or proposed blister drawing with cavity depth, radii, pitch, seal land, card size and cutting pattern;
- accepted output target tied to a named format, run duration, inspection scope and line boundary;
- feeding, inspection, reject tracking, coding, registration, perforation and discharge requirements;
- product-contact boundary, cleaning, line clearance, changeover and maintenance requirements;
- utilities, room conditions, access, ergonomics, safety and upstream/downstream interfaces; and
- drawings, manuals, certificates, FAT, qualification support, training and turnover-document scope.
Require the supplier to answer each testable requirement as comply, partial or deviation with an evidence reference. A statement that the machine “runs Alu-Alu and PVC” is not a sufficient response to the actual material and format matrix.
FAT
Prove the chosen package on the purchased configuration
Factory acceptance testing should use the approved or representative product, forming web, lidding and tooling whenever practical. Identify every material lot and machine, software, recipe and tooling revision. Agree the protocol and acceptance criteria before execution.
| FAT area | Evidence to retain | Decision supported |
|---|---|---|
| Forming | Settings, cavity measurements, visual defects and samples across positions and time. | The exact web can form the approved geometry within a justified window. |
| Feeding | Empty, double, damage, jam and intervention record under representative conditions. | The feeder can handle the product and format reproducibly. |
| Sealing | Controlled parameters, sampling, seal and integrity results, including interruptions. | The web and lidding pairing has a practical operating window. |
| Inspection/reject | Controlled challenge set, detection, tracking, rejection, confirmation and reconciliation. | Defined defects reach the correct disposition. |
| Coding/cutting | Registered samples, code results, card dimensions, perforation and cut quality. | The final card meets the drawing and information requirements. |
| Sustained output | Accepted packs, rejects, waste, stops, interventions and run time. | The integrated process meets the agreed output boundary. |
FAT supports equipment acceptance; it does not replace site qualification, process performance qualification or product stability work. Define which supplier evidence may be leveraged and which checks must be repeated after transport, installation and site integration.
Lifecycle control
Manage material and pack changes after launch
Changes to supplier, manufacturing site, resin, aluminum layer, coating, adhesive, primer, ink, thickness, cavity geometry, lidding, sealing window or machine tooling can affect the approved package. Require supplier change notification where appropriate and assess changes through the manufacturer’s quality system.
The impact assessment should consider material specifications, compatibility, forming, seal and integrity, artwork, stability, equipment qualification, process validation, regulatory filings and inventory transition. A change described as “equivalent” by a supplier may still affect the formed cavity or approved dossier.
Monitor routine rejects, forming defects, seal results, code and registration issues, line stops, roll variability, complaints and stability trends. Preserve retained samples and traceability sufficient to investigate. The material selection remains defensible only while the commercial system stays within its approved state.
Common mistakes
Avoid seven shortcuts that create false confidence
- Comparing names instead of specifications. “PVC” and “Alu-Alu” do not identify an exact supplier grade or complete pack.
- Copying generic barrier numbers. Values without aligned methods, conditions, structures and units cannot support a fair comparison.
- Using flat-film data as finished-pack proof. Forming, sealing and converting can introduce new failure modes.
- Choosing from climate alone. Market conditions inform stability; they do not create a universal material mandate.
- Ignoring card and carton geometry. A larger cavity footprint can change material use, output and distribution cost.
- Buying a machine before freezing the package. Material, drawing, feeder, tooling and inspection are interdependent.
- Treating FAT as product approval. Supplier testing cannot replace the manufacturer’s stability, qualification and release responsibilities.
Each shortcut can be prevented by a controlled input: exact materials, approved drawing, product-specific evidence, testable URS, agreed protocol and documented decision ownership.
Evidence hierarchy
Use primary standards and product-specific records in the right order
Regulations and guidance define principles and responsibilities. Consensus standards can define test methods. Supplier documentation identifies the material offered. Development studies and stability data connect the proposed package to the specific product. Equipment trials and qualification connect that pack to a repeatable manufacturing process.
No single layer replaces the others. A standard test method does not set the product’s acceptance criterion. A supplier data sheet does not approve a market pack. A passing machine trial does not establish shelf life. A stability batch does not prove every future material or process change.
Build traceability from product risks to package requirements, from requirements to material and drawing specifications, and from specifications to test records and approved conclusions. That structure makes the Alu-Alu versus PVC/Alu choice reviewable during development, procurement, transfer and later change control.
Frequently asked questions
Alu-Alu vs. PVC/Alu blister packaging FAQ
What is the main difference between Alu-Alu and PVC/Alu blister packaging?
Alu-Alu uses an opaque aluminum-containing cold-form laminate to make the cavity, while PVC/Alu uses a transparent PVC or PVC-based web that is heated and thermoformed. Both commonly use aluminum lidding, but their forming process, visibility, geometry, equipment and evidence requirements differ.
Is Alu-Alu always better than PVC/Alu?
No. Alu-Alu usually provides the stronger barrier position, but it is opaque and can require a larger cavity footprint, different tooling and a cold-form machine configuration. PVC/Alu preserves visibility and can be more compact. Product-specific stability and package requirements should decide.
Is Alu-Alu mandatory for humid or tropical markets?
Not as a universal rule. Climate, distribution and labeled storage conditions inform the stability strategy, but the approved package depends on the product, complete material structure, blister design and stability evidence for each intended market.
Which blister format provides better product visibility?
PVC/Alu normally allows the product to be viewed through the transparent PVC-based cavity. Alu-Alu is opaque, so product-presence and defect inspection generally need to occur before lidding or through another justified inspection strategy.
Can the same blister machine run Alu-Alu and PVC/Alu?
Some machine platforms can be configured for both cold forming and thermoforming, but compatibility must be confirmed for the exact model, installed modules, material grades, web width, blister drawing, tooling, feeder, inspection and accepted-output requirement.
How should barrier performance be compared?
Align the exact material structure, test method, temperature, humidity or pressure conditions, units, conditioning and specimen orientation. Then evaluate the formed and sealed blister with suitable package tests and the approved stability programme rather than relying only on flat-film values.
Which costs less, Alu-Alu or PVC/Alu?
There is no universal project cost. Compare forming and lidding material per accepted pack, card and carton size, machine configuration, tooling, output, waste, inspection, qualification, stability work, inventory and product-risk consequences using current supplier quotations and production evidence.
What should I send a machine supplier for a reliable proposal?
Send product drawings and samples, full forming and lidding specifications, the blister drawing, accepted-output target, inspection and coding scope, downstream interface, facility conditions, format matrix and documentation and qualification requirements.
Sources and next reading
Regulatory and technical references
These sources define stability, container-closure and test-method principles. Apply the current version and the requirements relevant to the product and intended markets.
Need a material-to-machine compatibility review?
Send the product drawing and samples, exact forming web and lidding specifications, proposed blister layout, accepted-output target and inspection, coding and qualification scope. HIJ can review the required process route and machine configuration before a quotation is prepared.
Technical review: Forester Xiang, HIJ Machinery. Final material, package, regulatory and validation decisions remain with the drug manufacturer and its authorized functions.