A useful defect investigation separates what you can see on the finished pack from the process stage that created it.
Use this guide to trace leaks, variable fills, contaminated seal lands, distorted cavities, registration errors, coding problems and material separation without changing several machine settings at once.
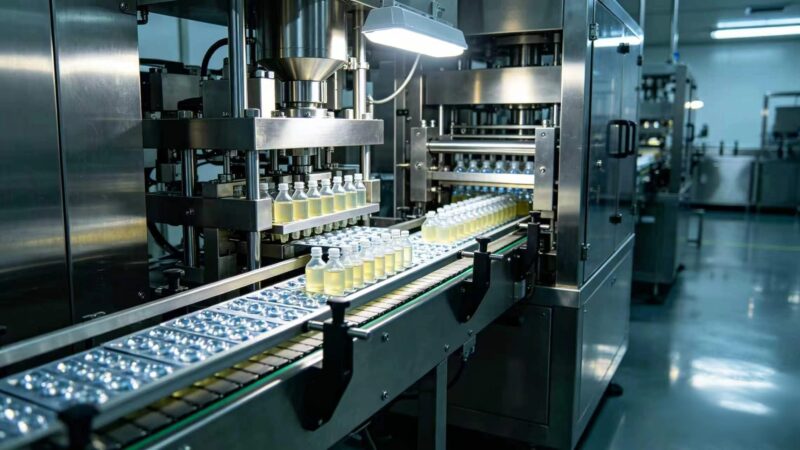
Important: this is a diagnostic framework, not a universal parameter sheet. Your approved temperature, pressure, dwell, fill target, sampling plan and package-integrity limits must come from the actual product–package system and its validation evidence.
Start with the defect pattern—not a random machine adjustment
A leak is an outcome, not a root cause. The same visible failure can begin with a damaged web, an unstable cavity, an off-center nozzle, product on the seal land, uneven sealing contact, incorrect registration or rough discharge handling. Record the pattern before touching the recipe.
Contain
Segregate affected output according to your quality procedure and preserve representative defect samples.
Describe
Record position, lane, cavity, time, material lot, recipe, product condition and whether the defect repeats.
Localize
Decide whether the pattern begins at unwind, forming, filling, lidding, sealing, coding, cutting or discharge.
Challenge
Change one justified variable at a time and compare against a retained reference—not against memory.
Lock
After confirmation, update the controlled recipe, inspection point, training or maintenance task.
Parameter second.
If failures repeat in the same lane or platen area, investigate the local mechanical, thermal or material path. If failures move with a material roll, product batch or tooling set, follow that variable. If they appear after a stop, restart or speed change, examine the transient condition rather than only steady-state production.
Trace the four failures that usually begin before final cutting
The practical question is not simply “what is the defect called?” It is “what evidence would distinguish a material problem from a forming, dosing or sealing problem?” Use the checks below as an investigation order, then apply your approved limits.
Seal leaks or channels
- Visible pattern
- Wet edges, loss of contents, a channel through the seal, weak or nonuniform bond, or failures concentrated in one platen area.
- Possible sources
- Contamination on the seal land, damaged lidding, wrinkles, poor web support, uneven contact, an unsuitable sealing window or a package-test method that cannot resolve the relevant leak.
- Check next
- Map the failure by cavity position; inspect seal-land cleanliness and flatness; compare actual temperature, pressure/contact and dwell records with the validated recipe; verify the test fixture and method.
Short, high or variable fill
- Visible pattern
- Underfilled pockets, overflow, splashing, weight or volume drift, bubbles, dripping nozzles or lane-to-lane variation.
- Possible sources
- Product temperature or viscosity change, air in the product path, inconsistent feed pressure, worn or incorrectly configured dosing parts, nozzle timing, poor cut-off or an unsuitable sampling method.
- Check next
- Review product condition and agitation; prime the complete path; inspect hoses, valves, seals and nozzles; compare each lane separately; confirm the measuring method and tare control.
Product on the seal land
- Visible pattern
- Residue, splashes, strings or droplets between the cavity and lidding, often followed by intermittent channels or stained foil.
- Possible sources
- Overfill, unstable nozzle position, late cut-off, product stringing or foaming, excessive acceleration, shallow headspace or motion between filling and sealing.
- Check next
- Observe the fill in slow motion; inspect nozzle centering and retraction; evaluate headspace and product behavior; verify transfer stability and the time between dosing and sealing.
Distorted, thin or inconsistent cavities
- Visible pattern
- Uneven depth, whitening, webbing, thin corners, collapsed pockets, poor flange flatness or a repeated cavity-volume difference.
- Possible sources
- Material variation, incorrect heating distribution, forming pressure or vacuum problems, tooling wear, poor cooling, web tension or an unsuitable cavity geometry.
- Check next
- Measure depth and flange flatness by position; compare material lots; inspect heater-zone readings and tooling condition; verify cooling and web support before changing downstream stations.
Finish the investigation through registration, lidding and material integrity
A pack can be well formed and accurately filled yet still fail because the web loses registration, the printed or coated lidding is mishandled, or the selected material system is not suitable for the product and distribution conditions.
Registration or punch misalignment
Look for off-center pockets, uneven margins, partial cuts, print-to-pocket drift or defects that accumulate after a stop or roll change. Possible sources include mark detection, pitch settings, traction, web tension, tooling registration and mechanical wear.
First evidence: mark-sensor status, index history, pitch samples and a position map across time.
Lidding, print or code defects
Wrinkles, unreadable codes, misplaced information, damaged foil or poor print adhesion can originate in roll handling, tension, print registration, ribbon/ink selection, dirty optics, recipe control or inspection/reject logic.
First evidence: approved artwork, roll direction, code recipe, readability samples and reject challenge results.
Layer separation or material damage
Delamination, cracking, stress whitening, corrosion or barrier failure needs a material-system investigation. Review product compatibility, forming stress, sealing exposure, storage and distribution—not only the machine set-point.
First evidence: supplier specification/COA, retained material, compatibility and stability data, plus a controlled comparison with an approved lot.

Use operating video and retained samples together: video helps connect the final defect to the exact station sequence, while samples preserve the physical evidence.
Use the defect pattern to choose the next inspection point
This table is a triage tool. It narrows the investigation; it does not prove the cause. Confirmation requires controlled checks with the approved product, material, tooling and test method.
| Observed pattern | Prioritize this path | Collect this evidence first | Avoid this shortcut |
|---|---|---|---|
| Same cavity position repeatedly leaks | Local seal contact, platen condition, tooling support, cavity flange or recurring contamination | Position map, pressure/contact film if applicable, thermal record, flange sample | Raising the global temperature before checking the local pattern |
| Failure moves with a material roll | Web or lidding damage, thickness, coating, roll direction, storage and supplier lot | Lot/COA, retained roll sample, incoming inspection, approved-lot comparison | Rebuilding machine settings around one unconfirmed material lot |
| Fill drifts during the run | Product condition, feed pressure, air, pump/valve/nozzle state and temperature | Time-series sample by lane, product temperature, recipe and stop/restart history | Averaging all lanes and hiding a single-lane problem |
| Defects start after stopping or restarting | Transient heating, product settling, trapped air, web relaxation, index and restart sequence | First packs after restart, alarm/event history and operator sequence | Evaluating only stable middle-of-run samples |
| Outer lanes fail more than center lanes | Cross-web heating, pressure/contact, tension, forming distribution or nozzle alignment | Lane-by-lane results and cross-web temperature/geometry map | Reporting one combined pass rate for the complete web |
| Print or punch slowly drifts | Registration mark, sensor cleanliness, pitch, traction, encoder and roll tension | Sequential samples, mark-sensor signal and index trend | Correcting the cutter without finding the upstream drift |
| Wrinkles appear near filled cavities | Web support, heat exposure, product contamination, lidding tension and cavity/flange geometry | Unfilled trial, filled trial, slow-motion observation and material comparison | Assuming the lidding roll alone is responsible |
| Package passes visual inspection but fails an integrity test | Microchannel, incomplete bond, test fixture, test sensitivity or sample conditioning | Known-good and known-defect controls, fixture check and method record | Treating appearance as proof of package integrity |
Change one variable
- State the hypothesis before the trial.
- Hold product, material and tooling constant where possible.
- Keep the previous sample and result.
- Repeat enough cycles to observe the actual pattern.
Escalate through your quality system when
- Package integrity or dose acceptance is not met.
- The cause is unknown or the correction is not repeatable.
- A material or tooling change may affect validated status.
- Affected output cannot be confidently bounded.
Put defect prevention into the URS, trials and FAT—not only the operator manual
A stable line needs an agreed boundary for the product, package, materials, machine sequence, inspection and evidence. Ask suppliers to quote and test the same inputs so that a “pass” means the same thing to every party.
Approved samples
Define representative liquid, viscosity/temperature range, foaming or stringing behavior, cavity drawing, lidding and forming materials.
Defect catalogue
Agree examples of leak, contamination, short fill, distortion, registration, coding and material defects before the acceptance run.
Recipe boundary
List controlled set-points, access levels, change authorization, alarm history and the conditions under which a recipe may be revised.
Inspection boundary
State what is checked online, what is sampled offline, the test method, challenge pieces, reject route and retained evidence.
Operating states
Test startup, stable run, planned stop, restart, roll splice, product refill, speed change and end-of-run—not only one short steady sample.
Acceptance basis
Define sample quantity, run duration, allowable conditions, disposition of defects and who approves the final result.


When a supplier is asked only for a headline speed, the discussion starts too late in the process. I would first ask for the actual liquid, cavity and material samples; then define the defect catalogue and the evidence that must leave FAT with the machine. That turns troubleshooting requirements into a purchase specification instead of an argument after installation.
Choose an integrity test that matches the package and the quality risk
Visual inspection, seal-quality testing and leak testing answer different questions. Define the defect you need to detect, whether the package is porous or nonporous, the relevant product risk, the fixture, sensitivity, controls and acceptance criteria before naming a method in the URS.
ASTM F2338-24
This is a nondestructive vacuum-decay leak-detection method—not a dye-ingress method. Applicability and sensitivity depend on the package, fixture and test parameters.
Review ASTM F2338-24 scopeUSP <1207>
USP describes package-integrity assurance for nonporous packages intended for sterile pharmaceutical products and emphasizes method selection and validation across the product life cycle.
Review the USP chapter overviewFDA packaging guidance
FDA’s container-closure guidance explains that tests and acceptance criteria should be scientifically justified for the specific packaging system and product.
Read the FDA guidanceDo not copy universal numbers from another project. Sealing windows, sampling frequencies, leak limits, dose tolerances and maintenance intervals must be established for the intended product–package system. Supplier trials support that work; they do not replace the buyer’s quality approval, validation, stability program or batch-release decision.
Liquid blister packaging defect FAQ
What usually causes a liquid blister package to leak?
Possible causes include product or debris on the seal land, lidding or forming-web damage, wrinkles, poor flange flatness, uneven sealing contact, an unsuitable process window or damage after sealing. Map the failures by cavity and time before changing parameters.
Should I increase sealing temperature when I find leaks?
Not automatically. More heat may not correct contamination, wrinkles, pressure/contact variation, damaged material or a poor test fixture, and it can narrow the operating window. Confirm the likely failure path and change one justified variable at a time.
Why does fill quantity drift during a production run?
Review product temperature and rheology, agitation, feed pressure, trapped air, pump or valve condition, nozzle cut-off, refill events, stops and the measurement method. Compare lanes separately and plot results over time.
What causes liquid to enter the seal area?
Overfill, splashing, foaming, stringing, nozzle misalignment, poor cut-off, unstable transfer or insufficient usable headspace can carry product onto the flange. Observe the complete fill-to-seal sequence rather than only the finished package.
How do I diagnose registration drift?
Keep sequential samples and review the registration mark, sensor condition and signal, pitch, traction, encoder feedback, roll tension and restart behavior. A gradual trend usually requires a different investigation from a sudden step change.
Is visual inspection enough to release liquid blister packs?
Visual inspection is valuable for visible damage, contamination, wrinkles, registration and gross seal defects, but it does not establish package integrity by itself. The appropriate integrity and seal-quality methods must be selected and validated for the intended package and product.
What should a liquid blister FAT include?
Use representative product and packaging materials; define defect examples, run states, sample quantities, acceptance criteria, inspection and reject challenges, records, responsibilities and the disposition of open items. Include stops, restarts and material handling—not only a short stable run.
What information should I send for troubleshooting support?
Send the product and material description, cavity drawing, machine model, recipe and recent changes, defect photos by position, retained samples, material lot, event history, inspection results and a short video showing the relevant station sequence.
Turn your defect evidence into a controlled investigation plan
Send the real product, materials, cavity drawing, defect pattern, current recipe, samples and required output. HIJ can review the machine sequence, likely inspection points and a project-specific trial or FAT scope.
About this technical guide: prepared for owners, engineers, quality teams and procurement staff evaluating liquid unit-dose blister processes. It supports troubleshooting and specification discussions but does not replace product-specific risk assessment, validation or quality approval.